Monday, May 22, 2024
Custom PCB Prototyping: Fast Turn Options and Common Trade-Offs
by
Published
Views:
Custom PCB prototyping is the fastest way to validate circuit performance before scaling to production, but speed often comes with trade-offs in cost, material choice, layer stack-up, and testing depth. For operators and technical users, understanding these fast-turn options is essential to balancing lead time, reliability, and manufacturing accuracy in today’s demanding electronics environment.
Across electronics, mobility systems, smart agricultural controls, environmental monitoring hardware, and industrial tooling, prototype boards often determine whether a project moves smoothly into pilot builds or stalls during validation. For users working close to assembly, testing, and field deployment, the right custom PCB prototyping strategy reduces rework, shortens debug cycles, and supports better procurement decisions.
Within a cross-sector benchmarking environment such as Global Industrial Matrix, prototype choices are rarely isolated. A board that works for a low-volume sensor node may fail under EV vibration, irrigation humidity, or industrial pump control heat loads. That is why fast-turn options must be reviewed not only by lead time, but also by stack-up realism, manufacturability, test coverage, and downstream compliance expectations.
Why custom PCB prototyping matters in modern industrial workflows
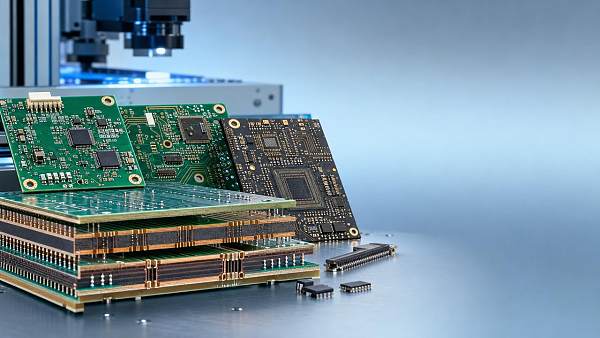
In practical terms, custom PCB prototyping bridges the gap between schematic intent and production reality. Operators rely on prototypes to verify solderability, connector fit, signal stability, thermal behavior, and assembly compatibility before a design reaches quantities of 100, 1,000, or more units.
A fast-turn prototype can arrive in 24 hours to 7 days, depending on layer count, surface finish, and drilling complexity. That speed is valuable when a controls board for an autonomous tractor, battery management unit, or filtration sensor needs immediate bench testing. However, the fastest option may exclude impedance control, advanced laminates, or full electrical test.
Common industrial use cases
Industrial users typically order custom PCB prototyping for 4 main reasons: first-article validation, firmware bring-up, enclosure fit checks, and process qualification. In mixed-sector manufacturing, these goals often overlap. A single board may need to survive vibration, moisture, current peaks, and connector cycling within the same validation program.
- Motor control and power conversion boards for automotive and mobility platforms
- Sensor acquisition and telemetry modules for agri-tech equipment
- Process control boards for water treatment, filtration, and environmental systems
- Interface and safety boards for precision tooling and factory automation
Where operators see the trade-offs first
The first warning signs usually appear on the shop floor or test bench. Warped panels, limited solder mask registration, missing test coupons, and substitute laminate choices can affect yield long before procurement identifies the root cause. In many projects, a 2-day acceleration at prototype stage can create a 2-week delay during troubleshooting if key build assumptions were not reviewed.
The table below outlines how fast-turn options usually compare in real industrial use, especially when operators must balance urgency against validation depth.
The key point is that fast custom PCB prototyping should match the stage of risk reduction. If the objective is only firmware boot-up, a simpler build may be enough. If the board will later support current loads above 20A, operate in 60°C ambient conditions, or interface with sensitive RF sections, the prototype must reflect those realities much earlier.
Fast-turn options and the most important technical trade-offs
Not all speed options are equal. In custom PCB prototyping, turnaround is influenced by at least 6 variables: layer count, board size, material type, copper weight, hole structure, and test requirements. Understanding how these variables interact helps users avoid prototype results that look acceptable on paper but fail under real operating stress.
Material selection: standard FR-4 versus application-driven laminates
For many quick-turn jobs, standard FR-4 with 1 oz copper and 1.6 mm thickness is the default. It is cost-efficient and widely available. Yet industrial devices exposed to thermal cycling, high switching frequency, moisture, or mechanical shock may require higher Tg material, heavy copper, or low-loss laminates even at the prototype stage.
Using a substitute laminate can reduce lead time by 1–3 days, but it may alter dielectric behavior, thermal expansion, or rigidity. That matters in automotive electronics, high-current pump drives, and sensor hubs installed outdoors for 12 to 24 months between maintenance intervals.
When standard material is usually acceptable
- Early logic validation and low-voltage digital control boards
- HMI interface boards with modest thermal load
- Fixture electronics used only in lab or factory settings
When material shortcuts create risk
- High-speed interfaces where impedance stability matters
- Power electronics above 48V or sustained current above 10A–20A
- Outdoor and humid applications in agriculture or infrastructure systems
Layer stack-up realism
A 2-layer prototype may validate basic functionality, but it rarely predicts EMI, return path quality, or thermal spreading in a 6-layer production design. In custom PCB prototyping, changing from a simplified stack-up to the final one can reveal new issues in noise coupling, via escape, and routing density.
For operators, the practical question is simple: does the prototype represent the production build closely enough to make test results meaningful? If not, early pass results can be misleading. This is especially true for HDI substrates, compact sensor modules, and inverter support boards.
Surface finish and assembly impact
Lead-free HASL is often faster and cheaper, while ENIG offers flatter pads for fine-pitch devices and more stable assembly outcomes. The difference matters when pad pitch drops below 0.5 mm or when the board includes BGAs, QFNs, or high-pin-count connectors. A lower-cost finish can be acceptable for through-hole validation, but it may distort results for dense SMT assemblies.
Testing depth versus schedule pressure
One of the most overlooked trade-offs in custom PCB prototyping is test coverage. Some urgent builds rely on sample-based continuity checks rather than 100% electrical test. That may save 12 to 24 hours, yet it increases the chance that users spend debugging time on manufacturing defects instead of design defects.
The following comparison helps operators align prototype speed with validation quality.
If the board is intended for regulated sectors, harsh environments, or cross-border procurement programs, the more robust path usually delivers lower total risk. The initial unit cost may rise by 10% to 30%, but the gain in troubleshooting accuracy often justifies that premium.
How operators should choose a prototype path
Choosing custom PCB prototyping successfully starts with defining what must be proven in the next build. Too many teams request the fastest possible delivery without specifying whether they need form verification, firmware readiness, thermal evidence, or near-production reliability. These are different objectives and require different build assumptions.
A 5-step decision process
- Define the validation target: function, assembly, stress, or certification preparation.
- List the 3 to 5 critical risks such as impedance, heat, connector wear, or vibration.
- Match the stack-up and material to the most important risk, not just the budget target.
- Confirm test depth, including electrical test, AOI, and sample cross-section if needed.
- Review whether the prototype data can support the next purchasing or engineering gate.
This process is especially useful in organizations where procurement, design, and operations work across multiple product categories. A board for an EV subsystem and a board for a nutrient dosing controller may both be called prototypes, yet their failure modes, environmental exposure, and acceptance criteria differ significantly.
Questions to ask before placing the order
Operators should verify 6 practical items before release: final layer count intent, target copper weight, board thickness tolerance, finish type, minimum trace and space, and required testing scope. In many cases, asking these questions early prevents a second prototype spin that adds 5 to 10 days and duplicates assembly effort.
- Will this board later require IPC-aligned documentation or traceability?
- Is panelization needed for SMT line efficiency or manual handling safety?
- Do mounting holes, connectors, and keep-out zones match the final enclosure revision?
- Will current density or thermal rise invalidate a simplified copper plan?
Procurement and cross-functional alignment
In a global manufacturing environment, custom PCB prototyping also supports sourcing decisions. If a supplier can deliver quickly but cannot maintain stack-up consistency, documentation discipline, or process transparency, the prototype may not be a reliable benchmark for future volume production. Speed alone is not a sourcing strategy.
Platforms that benchmark electronics against broader industrial standards help teams compare prototype choices in context. That is valuable when electronics must integrate with vehicle systems, agricultural equipment, environmental control packages, or precision machines that carry their own mechanical and compliance constraints.
Common mistakes, risk controls, and practical recommendations
The most common mistake in custom PCB prototyping is assuming that a functioning board is a validated board. A prototype may power on and pass basic I/O checks, yet still fail after 48 hours of thermal load, 200 connector insertions, or repeated exposure to dust and humidity. Industrial users need validation criteria that reflect actual service conditions.
Frequent mistakes
- Using a prototype stack-up that is too different from production intent
- Skipping full electrical test to save less than 1 day
- Approving material substitutions without checking thermal or dielectric impact
- Ignoring fixture access, test points, or assembly handling constraints
Risk control measures that add real value
A practical control plan includes 4 elements: DFM review, documented material confirmation, defined test coverage, and a feedback loop from assembly or field simulation. Even for rapid programs, these checks often add only a few hours to the release process while preventing days of avoidable debug effort.
For critical applications, operators should also retain fabrication notes, stack-up details, and revision history from each prototype run. That record supports more accurate root-cause analysis and creates a usable benchmark when procurement compares regional supply options or prepares for dual-source qualification.
What a well-planned prototype delivers
When planned correctly, custom PCB prototyping shortens the path to stable production by clarifying which issues belong to design, which belong to fabrication, and which belong to assembly or operating environment. That distinction matters in every industrial sector because it improves communication between engineering, sourcing, and operations teams.
For organizations navigating electronics within larger industrial systems, the strongest approach is not simply faster boards. It is better data from each board iteration, tighter alignment between prototype intent and production reality, and clearer evidence for go or no-go decisions.
Custom PCB prototyping works best when lead time, material choice, layer strategy, and testing depth are treated as linked decisions rather than isolated cost items. For operators and technical users, that means choosing a prototype path based on actual use conditions, verification goals, and supply chain continuity. If you need a more structured way to compare prototype options across electronics, mobility, agri-tech, infrastructure, or tooling programs, contact GIM to get a tailored benchmarking perspective, discuss your build requirements, and explore more solutions.
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.