Monday, May 22, 2024
IPC-Class 3 Compliance Checklist for High-Reliability PCB Assembly
by
Published
Views:
For quality control and safety managers, ipc-class 3 compliance is more than a certification target—it is a practical safeguard for mission-critical PCB assembly. This checklist-driven guide outlines the key inspection, documentation, process control, and reliability requirements needed to reduce defects, strengthen traceability, and align high-reliability electronics production with stringent IPC expectations.
What does ipc-class 3 compliance actually mean in high-reliability PCB assembly?
In practical terms, ipc-class 3 compliance refers to meeting the most stringent workmanship and reliability expectations defined by IPC standards for electronic assemblies used in life-critical, safety-critical, or mission-critical environments. These products are expected to continue functioning when failure is not acceptable, such as in aerospace controls, medical electronics, industrial safety systems, rail infrastructure, defense hardware, and other harsh-duty applications.
For quality teams, this is not simply about making boards look cleaner under magnification. It is about controlling the full manufacturing system: material traceability, process capability, solder joint integrity, cleanliness, operator qualification, inspection evidence, and rework discipline. A board can pass basic electrical testing and still fall short of ipc-class 3 compliance if documentation is weak, hole fill is insufficient, solder wetting is marginal, or contamination risk is unmanaged.
This matters across the broader industrial ecosystem that Global Industrial Matrix analyzes, because high-reliability PCB assembly increasingly supports interconnected sectors. A controller used in EV charging infrastructure, a precision sensor node in smart agriculture, or an environmental treatment monitoring module may all require a reliability mindset similar to traditional aerospace programs. The standard therefore acts as a cross-sector quality benchmark, not a niche label.
Which products and operations should prioritize ipc-class 3 compliance first?
Not every product requires the cost and control intensity of Class 3, but many organizations underestimate where the risk threshold begins. Quality control and safety managers should prioritize ipc-class 3 compliance when electronic failure could create any of the following consequences:
- Safety hazards to operators, patients, drivers, or the public
- Loss of critical monitoring or control functions
- High field repair cost due to inaccessible installation sites
- Regulatory exposure, audit failure, or contractual nonconformance
- Severe brand damage caused by early-life reliability failures
Typical examples include power control boards, braking or steering support electronics, battery management assemblies, industrial protection relays, filtration automation controllers, and ruggedized communication modules. In these cases, ipc-class 3 compliance is often less expensive than the long-term consequences of latent defects.
A useful internal screening question is this: if this PCB assembly fails in service, will the problem be merely inconvenient, or will it disrupt a critical function, trigger unsafe behavior, or require costly emergency replacement? If the answer points toward risk concentration, Class 3 review should begin early in design transfer and supplier qualification.
What should be on an ipc-class 3 compliance checklist for QC and safety managers?
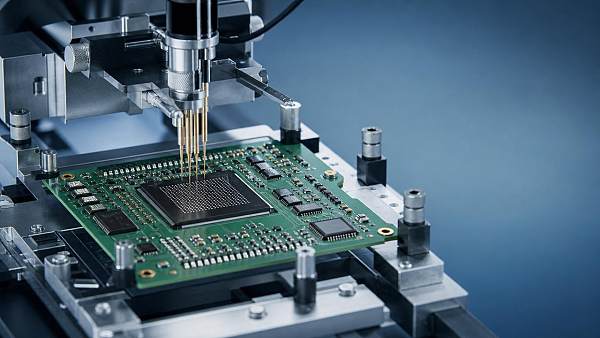
A strong checklist should not be limited to final visual acceptance. It should connect incoming materials, assembly execution, inspection logic, and release documentation. The most effective ipc-class 3 compliance checklists are stage-based and auditable.
1. Material and traceability controls
- Laminates, solder paste, flux, components, and finishes are approved and revision-controlled
- Lot codes and date codes are traceable to each production batch
- MSD handling, storage conditions, and shelf-life controls are documented
- Incoming inspection criteria are aligned with high-reliability requirements
2. Process setup and validation
- Stencil design, paste volume, placement accuracy, and thermal profile are validated
- Wave, selective, or hand soldering parameters are standardized and recorded
- Critical process windows are defined with alarms or response limits
- Operator certifications and workmanship training are current
3. Inspection and workmanship verification
- Solder fillets, wetting, heel coverage, lead protrusion, and void-related criteria are checked to applicable IPC documents
- Through-hole fill and barrel integrity meet Class 3 expectations
- AOI, X-ray, and manual visual inspection points are risk-prioritized
- Accept/reject examples are documented for consistent inspector judgment
4. Reliability and contamination controls
- Cleaning method and residue limits are verified for the product environment
- Conformal coating, bonding, staking, or underfill processes are validated where required
- Thermal cycling, vibration, burn-in, or functional stress tests are considered based on end use
- ESD and handling controls are monitored continuously
5. Documentation and release evidence
- Traveler records, deviations, repairs, and concessions are complete
- Test reports and inspection records are linked to serial or lot identity
- Nonconformance trends are reviewed for systemic corrective action
- Final release is based on objective evidence, not informal judgment
How is ipc-class 3 compliance different from lower assembly classes?
The biggest difference is not just tighter workmanship limits; it is lower tolerance for risk. Lower classes may permit conditions that are still functional for consumer or general service products, while Class 3 assumes the assembly must survive more demanding environments with less room for degradation. That shifts the standard from “acceptable performance” to “high assurance performance.”
For procurement, engineering, and compliance leaders, this distinction is crucial. If a supplier claims to build “to IPC standards,” that phrase alone is too vague. The right question is whether the supplier’s documented controls truly support ipc-class 3 compliance for the specific assembly technology, environment, and reliability profile involved.
What are the most common mistakes companies make when pursuing ipc-class 3 compliance?
One frequent mistake is treating the requirement as a final inspection exercise rather than a process system. By the time a defect becomes visible at the end of the line, the cost of containment, rework, delay, and confidence loss is already high. True ipc-class 3 compliance is built upstream through design-for-manufacturing review, material discipline, validated profiles, and trained human judgment.
Another mistake is relying on generic supplier declarations. A contract manufacturer may have experience with high-reliability work, but quality managers still need evidence of actual capability: defect history, workmanship criteria, training records, X-ray coverage strategy, cleanliness verification, and rework authorization logic. “We can build Class 3” is not the same as “we can consistently demonstrate Class 3 controls.”
A third issue is weak deviation management. In high-reliability electronics, undocumented substitutions, informal touch-up, or acceptance based on schedule pressure can undermine the whole control framework. Safety managers should pay close attention to concession pathways, engineering approvals, and root-cause closure for recurring nonconformances.
Finally, some teams ignore the operating environment. Vibration, humidity, corrosive exposure, temperature cycling, and service-life expectations all influence what “compliant enough” means in real life. Even when workmanship passes, reliability can still fail if environmental assumptions were incomplete.
How can QC and safety managers verify a supplier’s ipc-class 3 compliance readiness before approval?
The most reliable approach is to combine document review, on-site audit logic, and pilot-build evidence. Start by asking for the supplier’s applicable IPC training records, workmanship acceptance criteria, process flow, inspection plan, and traceability method. Then verify whether those controls are actually used on the shop floor, not just stored in a quality manual.
During supplier evaluation, focus on how the factory handles edge cases. Ask how they manage insufficient hole fill, solder void concerns, mixed-technology boards, BGA hidden joints, coating defects, or repeated hand-solder interventions. Their answers will reveal whether they operate with disciplined escalation or informal problem-solving.
A good readiness review should also examine measurable indicators:
- First-pass yield on comparable high-reliability assemblies
- Defect escape rate and customer-return trends
- Calibration and maintenance compliance for critical equipment
- Cleanliness testing or ionic contamination control methods
- Corrective action closure speed and recurrence prevention
For organizations managing global supply chains, this verification step is especially important. Across electronics, mobility, agri-tech, and infrastructure systems, a small weakness in PCB assembly governance can cascade into field failures, warranty exposure, or delayed deployment at scale.
What is the smartest way to implement ipc-class 3 compliance without slowing production too much?
The answer is not to inspect everything more aggressively in an unstructured way. The smarter path is to design a risk-based control model. Start by identifying assemblies where failure consequence, service difficulty, and environmental stress justify Class 3 rigor. Then align inspection intensity and documentation depth with those risk drivers.
Next, strengthen process capability so the line naturally produces fewer borderline conditions. That means profile optimization, fixture control, solderability management, feeder accuracy, and clear workmanship libraries. When process variation is reduced at the source, ipc-class 3 compliance becomes more sustainable and less dependent on downstream sorting.
Digital traceability also helps. Linking lot data, machine parameters, inspection images, and repair records makes audits faster and root-cause analysis more credible. For industrial leaders balancing quality and throughput, this is where operational efficiency and compliance no longer conflict.
Most importantly, create a shared decision language between quality, manufacturing, engineering, and sourcing. Class 3 outcomes degrade when each function works from different assumptions about acceptability, urgency, or risk ownership. A common checklist and escalation path prevent that drift.
What should you confirm first if you are evaluating a program, supplier, or new production launch?
Before moving into production, approval, or supplier commitment, confirm a short set of high-value questions. Are the product’s end-use risks serious enough to require ipc-class 3 compliance? Which IPC documents and acceptance criteria apply to this exact assembly type? What evidence proves the supplier can repeat those controls under normal production volume, not just sample builds? How will traceability, nonconformance handling, and repair authorization be documented? And what reliability tests or environmental assumptions support the release decision?
For quality control and safety managers, these questions are often more important than unit price alone. They reveal whether a PCB assembly program is built on durable process discipline or on optimistic assumptions. If you need to move toward implementation, procurement, or technical benchmarking, the best next discussion points are specific process capability data, inspection criteria, pilot-run results, documentation depth, expected lead time, and escalation ownership for any Class 3-related deviation.
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.