Monday, May 22, 2024
PCB Assembly Metrics Analysis: Yield, DPMO, and Rework Benchmarks
by
Published
Views:
PCB assembly metrics analysis is essential for quality and safety teams seeking to reduce defects, control process variation, and improve production reliability.
In complex global manufacturing, yield, DPMO, and rework rates reveal whether electronics operations are stable, scalable, and aligned with IPC, ISO, and IATF expectations.
This guide explains how PCB assembly metrics analysis supports cross-industry benchmarking, from automotive control boards to industrial sensors and environmental monitoring hardware.
What does PCB assembly metrics analysis actually measure?
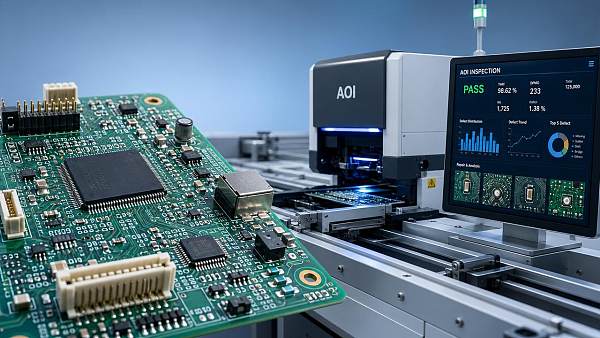
PCB assembly metrics analysis measures process output, defect frequency, repair burden, and production consistency across SMT, THT, inspection, test, and final verification stages.
Three indicators dominate most benchmarking systems: first pass yield, DPMO, and rework rate.
First pass yield shows how many assemblies pass without repair. DPMO estimates defects per million opportunities. Rework rate tracks how often units need correction.
Together, these metrics expose hidden instability that shipment volume alone can mask.
A factory can hit delivery targets while still suffering from solder voiding, tombstoning, polarity errors, insufficient wetting, or test escapes.
PCB assembly metrics analysis turns those issues into comparable data points.
Core definitions used in benchmarking
- Yield: percentage of boards meeting criteria at a defined process step.
- First pass yield: assemblies accepted without touch-up or repair.
- DPMO: defects normalized against total defect opportunities.
- Rework rate: share of assemblies needing corrective intervention.
- Escape rate: defects found after the intended inspection stage.
Why are yield, DPMO, and rework benchmarks so important?
Yield alone can look healthy while cost and field risk continue rising. That is why PCB assembly metrics analysis should never rely on one number.
A line with 98% final yield may still show excessive manual touch labor, retest loops, and latent reliability concerns.
DPMO helps compare unlike products. High-mix electronics often contain very different component counts, package types, and inspection opportunities.
Without normalization, one assembly line may appear worse simply because it builds denser boards.
Rework benchmarks matter because every solder touch increases thermal exposure, handling risk, and cycle time.
For automotive, infrastructure, and industrial control electronics, rework also raises traceability and audit questions.
What strong benchmark ranges often look like
Benchmarks vary by product complexity, compliance level, and production maturity. Still, practical ranges can guide early assessment.
These values are not universal pass or fail limits. PCB assembly metrics analysis must always consider product class, test depth, and reliability expectations.
How should different industries interpret PCB assembly metrics analysis?
Cross-sector electronics programs rarely tolerate the same defect profile. Interpretation depends on failure impact, maintenance access, and regulatory exposure.
Automotive boards may prioritize traceability, solder joint robustness, and zero-defect containment. Smart agriculture hardware may balance ruggedness with environmental exposure and cost discipline.
Industrial ESG infrastructure often emphasizes uptime, sensor integrity, and long service intervals.
PCB assembly metrics analysis is valuable because it creates a common language across these applications.
Scenario-based interpretation
- High-density control boards: DPMO trends may matter more than raw defect counts.
- Safety-related assemblies: rework controls and escape prevention become critical.
- Outdoor electronics: low initial defects are important, but process consistency matters even more.
- Prototype-to-ramp programs: yield learning curves should be measured weekly.
What mistakes make PCB assembly metrics analysis misleading?
The most common mistake is using inconsistent defect opportunity definitions. If one site counts every solder joint and another counts placements only, DPMO becomes distorted.
Another issue is mixing cosmetic and functional defects without weighting or categorization.
PCB assembly metrics analysis should separate severity classes, root cause groups, and escape stages.
A third mistake is measuring final yield after extensive hidden rework. That practice inflates apparent capability and masks chronic instability.
Data latency also creates risk. Monthly reports arrive too late for stencil, paste, placement, or profile corrections.
Common interpretation traps
How can teams improve yield and reduce DPMO without creating more rework?
Improvement starts with process discipline, not inspection volume alone. More inspection can catch defects, but it does not eliminate root causes.
PCB assembly metrics analysis becomes actionable when linked to printer capability, placement accuracy, oven profile control, and operator handling practices.
Priority actions with high practical impact
- Separate defects by process origin, not only by symptom.
- Review first pass yield by shift, product family, and line.
- Use SPI, AOI, AXI, and ICT data as a connected chain.
- Set rework authorization rules for high-reliability assemblies.
- Audit component moisture control, storage, and lot traceability.
- Correlate recurring defects with design-for-manufacturing limitations.
In many cases, a small stencil aperture adjustment or feeder maintenance routine lowers DPMO faster than broad retraining campaigns.
That is why PCB assembly metrics analysis should connect engineering evidence with daily execution data.
How do you build an audit-ready benchmarking system for long-term control?
An audit-ready system needs stable definitions, version control, and traceable escalation thresholds.
PCB assembly metrics analysis should be documented in a way that survives product transfers, supplier changes, and capacity expansion.
Useful systems align internal dashboards with external standards such as IPC workmanship criteria, ISO quality controls, and IATF evidence discipline.
Recommended control structure
- Define metric formulas and defect opportunity rules in one controlled document.
- Set alert levels for yield drop, DPMO spikes, and rework drift.
- Keep board family benchmarks separate from line-wide averages.
- Link corrective actions to measurable closure dates and owners.
- Retain evidence for trend reviews, audits, and supplier discussions.
Global Industrial Matrix supports this discipline by framing benchmark data across electronics, mobility, agri-tech, infrastructure, and precision manufacturing environments.
That broader view helps organizations compare PCB assembly metrics analysis against real operating conditions, not isolated factory snapshots.
Quick FAQ table: what should be checked first?
Effective PCB assembly metrics analysis does more than report defects. It reveals whether a manufacturing system is truly under control.
When yield, DPMO, and rework benchmarks are interpreted together, improvement priorities become clearer, audit readiness improves, and reliability risk becomes easier to manage.
The next practical step is to standardize metric definitions, benchmark by product family, and connect every recurring defect to a verified process cause.
That approach turns PCB assembly metrics analysis into a durable decision tool for global manufacturing performance.
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.