Monday, May 22, 2024

PCB Assembly Metrics Optimization for Better First-Pass Yield
by
Published
Views:
For quality and safety managers, PCB assembly metrics optimization is more than a production target—it is a disciplined approach to improving first-pass yield, reducing defect escape, and strengthening process stability. By tracking the right indicators across materials, soldering, inspection, and operator performance, manufacturers can turn scattered shop-floor data into measurable gains in reliability, compliance, and operational control.
What does PCB assembly metrics optimization actually mean?
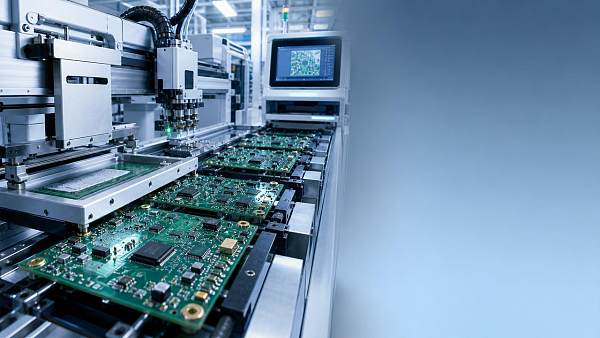
PCB assembly metrics optimization means selecting, validating, and improving the indicators that best predict assembly quality and repeatability.
It is not only about counting defects after production. It focuses on controlling upstream and in-process variables before failures multiply.
In electronics manufacturing, first-pass yield is a key result. However, yield alone cannot explain why a line performs well or poorly.
Effective PCB assembly metrics optimization links cause and effect across solder paste printing, component placement, reflow, inspection, rework, and final testing.
Within a cross-industry environment, this discipline also supports benchmarking. GIM aligns process evaluation with IPC guidance, ISO methods, and practical factory data.
That matters because electronics quality increasingly affects automotive systems, smart agriculture controls, water treatment automation, and industrial infrastructure.
Core metrics usually include:
- First-pass yield by line, product family, and shift
- Defect per million opportunities and defect escape rate
- Solder paste transfer efficiency and print repeatability
- Pick-and-place accuracy and feeder-related stoppage frequency
- Reflow thermal profile stability and solder joint defect trend
- AOI, SPI, AXI, and ICT false-call versus true-defect ratios
Which metrics most influence better first-pass yield?
The most useful metrics are the ones closest to defect creation. They should detect variation earlier than final electrical test.
Solder paste inspection often provides the earliest warning. Insufficient volume, offset, and bridging risk strongly affect downstream yield.
Placement quality is another leading indicator. Misalignment, component skew, nozzle wear, and feeder inconsistency often precede soldering defects.
Reflow profile control matters because temperature drift changes wetting quality, voiding behavior, and component stress exposure.
Inspection metrics must also be interpreted carefully. High defect counts do not always mean poor production if the system catches issues early.
A stronger signal is the ratio between in-line catches and end-of-line failures. Late discovery usually indicates weak process discipline.
High-impact indicators for PCB assembly metrics optimization:
- SPI volume deviation trend by pad category
- Placement offset distribution by package type
- Reflow peak and time-above-liquidus consistency
- AOI confirmed defect rate after review
- Rework frequency per board revision
- Final test failure mode recurrence
When these metrics move together, root cause analysis becomes faster. That is the practical value of PCB assembly metrics optimization.
How should metrics differ across products and industries?
Not every board should be measured in the same way. Product criticality, density, and operating environment change the right priorities.
Automotive control units may emphasize traceability, solder joint reliability, and process capability under IATF-aligned quality systems.
Industrial infrastructure boards may focus on long-life thermal stability, contamination control, and field-failure prevention.
Smart agriculture electronics often face vibration, moisture, and dust exposure. Here, conformal coating readiness and cleaning quality become more relevant.
High-density semiconductor-related assemblies require tighter attention to warpage, fine-pitch print quality, and hidden-joint inspection performance.
PCB assembly metrics optimization works best when metrics are weighted by product risk, not copied from another factory dashboard.
What common mistakes weaken PCB assembly metrics optimization?
A frequent mistake is chasing too many metrics. Large dashboards often create noise instead of actionable insight.
Another mistake is relying only on lagging indicators. Scrap and returns matter, but they appear after value has already been lost.
Some factories compare lines without normalizing for product mix. That produces unfair conclusions and weak corrective actions.
False-call rates are often ignored. If inspection systems over-report, teams may miss real failures among repeated review tasks.
Manual data entry is another risk. Delays, inconsistency, and selective logging damage the credibility of any optimization effort.
PCB assembly metrics optimization also fails when ownership is unclear. Every metric should have a responsible process owner.
Warning signs to watch:
- Stable FPY with rising field returns
- Low defect counts but high rework touch time
- Strong AOI performance but repeated ICT failures
- Good average results hiding high shift-to-shift variation
- Corrective actions that close quickly but recur often
How can implementation balance cost, speed, and measurable results?
The best approach starts small but structured. Begin with one line, one product family, and a short list of high-confidence indicators.
A practical pilot usually includes SPI trends, placement accuracy, reflow stability, confirmed AOI defects, and first-pass yield.
Use existing equipment outputs before investing in new systems. Many improvements come from better correlation, not more sensors.
Review metrics weekly at first. Daily reviews may be useful for unstable lines, but excessive reporting can reduce problem-solving time.
Set thresholds that trigger investigation. Avoid reacting to every single fluctuation unless the process is known to be highly sensitive.
For enterprise benchmarking, GIM-style cross-sector comparison is helpful. It reveals whether variation is local, product-specific, or structurally systemic.
Suggested rollout sequence:
- Map defect modes to process steps
- Choose five to seven leading and lagging metrics
- Define owners, data source, and review frequency
- Run a 30 to 60 day pilot
- Validate correlation with first-pass yield improvement
- Standardize and expand to other lines
Which quick-reference questions help evaluate success?
A compact FAQ table helps keep PCB assembly metrics optimization focused on decisions, not just reporting volume.
PCB assembly metrics optimization delivers the most value when metrics are few, relevant, and tied to clear process actions.
Better first-pass yield comes from disciplined measurement, fast interpretation, and standards-based benchmarking across product categories.
A practical next step is to audit current indicators, remove low-value reports, and build one pilot dashboard around defect prevention.
With a structured framework and verifiable technical data, PCB assembly metrics optimization can strengthen reliability, compliance, and operational resilience.

The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.