Monday, May 22, 2024

SMT Quality Standards Checklist for Consistent Line Performance
by
Published
Views:
Consistent SMT line performance starts with disciplined execution of SMT quality standards at every stage, from material control to placement accuracy and reflow verification. For operators and line users, a practical checklist reduces defects, improves traceability, and keeps daily production aligned with IPC and customer expectations. This guide highlights the essential control points that support stable output, higher yield, and reliable product quality.
Why do SMT quality standards matter so much on mixed-industry production lines?
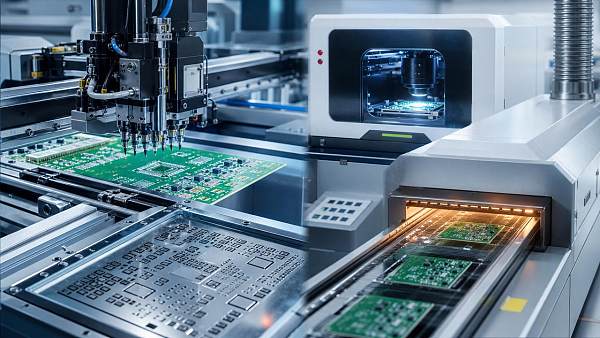
SMT quality standards are not only a compliance topic. For operators, they are the daily rules that prevent misplacement, soldering defects, material mix-ups, and hidden reliability failures. In cross-sector manufacturing, one line may support electronics for mobility, industrial controls, agri-tech devices, or environmental monitoring systems. That makes process discipline even more important.
A stable SMT line depends on repeatable inputs, controlled machine settings, verified outputs, and clear escalation rules. If any checkpoint is weak, yield loss often appears first as minor variation and then grows into expensive rework, delayed shipments, or field risk. Operators need a checklist that is simple to follow but strict enough to match IPC, customer drawings, and internal process windows.
Global Industrial Matrix (GIM) supports this need by connecting SMT quality standards with wider benchmarking across electronics, automotive-grade expectations, tooling capability, and compliance frameworks. That cross-industry view helps users understand why some controls are mandatory for one program and only recommended for another.
- Operators gain clearer pass/fail criteria for printing, placement, reflow, and inspection.
- Production supervisors improve traceability when lots, feeder data, profiles, and defect records are linked.
- Procurement and engineering teams reduce risk by aligning consumables, PCB requirements, and process capability with actual line conditions.
What should an operator include in an SMT quality standards checklist?
A practical checklist should cover the full line, not only AOI results or final appearance. Many recurring defects begin earlier, especially in storage, stencil condition, paste handling, feeder setup, and board support. The table below summarizes the core checkpoints that operators should review during startup, changeover, and routine production.
This checklist reflects the most common control points behind stable SMT quality standards. It also shows a key reality for operators: quality does not begin at final inspection. The strongest gains usually come from upstream controls that keep variation from entering the line.
Daily line-start checklist
- Confirm released work order, correct BOM revision, and approved machine program.
- Check stencil ID, cleanliness, and tension status if applicable.
- Verify solder paste batch, thawing completion, and remaining usable time.
- Review first-board print quality before placement starts.
- Cross-check feeder setup against program and component labels.
- Confirm reflow recipe and board support settings match product requirements.
- Record first article inspection results and escalate any trend before volume release.
Which process controls have the biggest impact on consistent line performance?
Not every checkpoint carries the same risk. In most SMT environments, four controls create the largest effect on line stability: solder paste management, print consistency, component placement accuracy, and reflow profile verification. When operators control these well, many downstream defects drop naturally.
1. Material and moisture control
Components exposed beyond their moisture floor life can crack, delaminate, or show latent reliability issues after reflow. This is especially important for fine-pitch ICs, BGAs, and high-value assemblies used in mobility electronics or industrial controls. Operators should treat label checking and floor-time recording as a quality action, not a warehouse task.
2. Solder paste and stencil discipline
Many visible defects start with unstable printing. Paste that is too cold, overworked, contaminated, or beyond its working life will change transfer efficiency. A dirty stencil underside can cause repeated bridging or insufficient deposits in the same board area. SMT quality standards therefore require documented handling rules, not casual judgment.
3. Placement verification beyond machine alarms
A line can continue running while still drifting out of control. Feeder wear, nozzle damage, poor board support, and incorrect component data can create small offsets before alarms appear. Operators should monitor recurring vision corrections, pickup misses, and skew patterns. Those are early warnings of capability loss.
4. Reflow profile confirmation
Using the wrong recipe can damage components or create weak solder joints. Even with the correct recipe, a profile should reflect actual board mass, copper distribution, and component sensitivity. For products crossing sectors such as automotive-adjacent electronics or outdoor environmental devices, thermal margin and solder joint reliability deserve extra attention.
How should operators judge defects under SMT quality standards?
Operators often face a difficult question: is this board truly defective, borderline, or only cosmetically different? A useful method is to combine customer criteria, IPC-based workmanship expectations, and process trend data. This avoids both over-rejecting acceptable boards and releasing risky ones.
The table below helps line users distinguish process signals that need immediate action from conditions that may only require observation or engineering review.
This type of comparison is useful because SMT quality standards are not enforced by one machine alone. They rely on decisions made by people at the line. Good operators read defects as process messages, not isolated events.
What do procurement and operations teams need to align before line release?
Operators often carry the burden of poor upstream decisions. A line may struggle not because execution is weak, but because material packaging is inconsistent, PCB warpage is not controlled, stencil design is unsuitable, or component substitutes were approved without process review. That is why SMT quality standards should connect procurement, engineering, and production.
Key alignment points before production
- Confirm alternate parts against footprint, coplanarity, termination finish, and packaging compatibility, not only electrical equivalence.
- Review PCB finish, pad definition, thickness, and warpage tendency for the intended thermal profile.
- Check whether the stencil aperture design matches fine-pitch, BTC, or large thermal-pad components.
- Verify if customer expectations require stricter workmanship classes, traceability depth, or process validation records.
This is where GIM adds practical value. By benchmarking assemblies and process expectations across electronics, mobility systems, infrastructure devices, and precision tooling environments, GIM helps users understand whether a sourcing choice is likely to reduce cost or create hidden production instability.
How can line users implement SMT quality standards without slowing output?
A common concern is that stricter controls reduce throughput. In reality, the opposite is usually true. When standards are built into routine actions, line stoppages become shorter, changeovers become cleaner, and repair loops become smaller. The goal is not more paperwork. The goal is faster decisions with fewer surprises.
Implementation steps that work on active lines
- Define critical-to-quality checkpoints for each product family, such as fine-pitch control, BGA inspection path, or high-thermal-mass profile verification.
- Limit checklist items to actions operators can actually verify on shift, with clear escalation if results fall outside the approved window.
- Use first-piece confirmation, mid-run sampling, and end-of-lot review rather than relying only on final AOI.
- Link defect records to feeder position, lot number, paste batch, and machine program so recurring causes are visible.
- Train operators to recognize trend signals such as rising false calls, repeated touch-up areas, or profile-sensitive defects after changeover.
For mixed-industry programs, implementation should also reflect product criticality. A consumer device board and a control module used in harsher environments may run on similar equipment, but they should not always use the same inspection depth, traceability record, or hold criteria.
Common mistakes operators should avoid
- Treating AOI as the only quality gate instead of checking print and placement stability upstream.
- Assuming a machine recipe is correct because the product code looks familiar during a fast changeover.
- Using substitute parts without confirming package tolerance, reel orientation, or reflow sensitivity.
- Ignoring minor but repeated defects because single-board fallout appears low.
- Recording rework without a defect reason code, which removes the chance to trace recurring process loss.
Each of these mistakes weakens SMT quality standards in a different way. Some increase scrap directly. Others damage traceability and delay root-cause analysis until a customer complaint or audit reveals the gap.
FAQ: practical questions about SMT quality standards
How often should SMT quality standards be reviewed on the line?
Review frequency should match risk. At minimum, operators should verify key SMT quality standards at startup, after changeover, when a material lot changes, and when defect trends shift. Higher-risk products may need additional in-process verification each shift or by lot size.
Which standards are most relevant for SMT operators?
Operators usually work closest to workmanship and process-control requirements tied to IPC documents, customer specifications, internal control plans, ESD rules, and traceability procedures. The exact list depends on product type, but the main point is to know which documents define acceptance and which define how the line must be controlled.
Can a tighter checklist reduce rework without hurting cycle time?
Yes, if the checklist focuses on high-impact items. A short checklist built around paste condition, print verification, feeder confirmation, recipe selection, and first-piece approval often saves more time than it consumes. It prevents long repair loops and repeated defect sorting later.
What should users do if customer criteria conflict with normal factory practice?
Follow the approved customer requirement and escalate the mismatch immediately. Do not rely on verbal habits or previous jobs. In multi-sector manufacturing, customer-specific workmanship, traceability, or inspection requirements can differ significantly even when the assemblies look similar.
Why choose us for SMT quality standards benchmarking and implementation support?
GIM helps operators, engineers, and sourcing teams turn SMT quality standards into usable line controls. Our advantage is not a single-product viewpoint. We connect electronics process discipline with cross-sector benchmarking in automotive and mobility systems, smart agri-tech hardware, industrial ESG infrastructure, and precision tooling environments.
That matters when your challenge is not just one defect, but the broader question of what should be controlled, documented, substituted, approved, or escalated across different product families. We support practical decisions around parameter confirmation, material and package suitability, process capability expectations, delivery-risk review, traceability depth, and certification-related production requirements.
- Consult us for SMT quality standards checklist design by product family or risk level.
- Ask for support with parameter confirmation, stencil and material compatibility review, and alternate-part risk screening.
- Discuss delivery timing, pilot-run planning, traceability expectations, and customer or IPC-aligned control points.
- Request guidance on sample evaluation, defect pattern interpretation, and cross-industry benchmarking before scaling production.
If your line needs clearer acceptance criteria, more reliable startup control, or better alignment between procurement and production, GIM can help define the right SMT quality standards framework for your application and operating reality.

The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.