Monday, May 22, 2024
When tech hardware prototypes fail, the issue is rarely the part
by
Published
Views:
When tech hardware prototypes fail, the root cause is often hidden in process integration, not the part itself. From PCBA manufacturing and tooling solutions to plastic injection mold factory coordination, modern manufacturing depends on aligned engineering standards, supplier discipline, and global manufacturing visibility. For teams balancing industrial infrastructure, industrial sustainability, and even crop monitoring systems, early benchmarking turns costly surprises into controlled, scalable outcomes.
Why prototype failure is usually a system problem, not a component problem
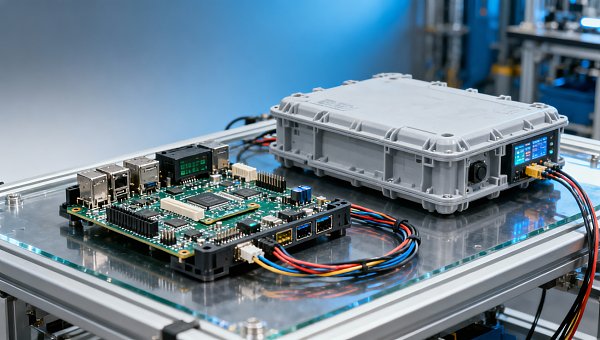
In cross-sector manufacturing, a failed prototype rarely points to one bad part alone. More often, the breakdown starts at the interface between design intent, process capability, supplier interpretation, and inspection criteria. A connector may pass incoming checks yet fail in vibration testing because board stack-up, fastening torque, enclosure tolerance, and thermal cycling were never benchmarked together during the first 2–4 weeks of prototype planning.
This issue is especially visible in programs that cross electronics, mobility, agri-tech, and environmental infrastructure. A subsystem that performs well in a lab may become unstable in field use when humidity ranges move from 40% to 85%, operating temperatures shift from 10°C to 45°C, or assembly variance exceeds a practical ±0.2 mm to ±0.5 mm window. The part did not suddenly become defective; the surrounding process was never fully aligned.
For operators, project managers, quality leaders, procurement teams, and financial approvers, this distinction matters. Replacing parts after every pilot build adds cost without solving root causes. A better approach is to audit the full prototype chain: design release, BOM maturity, tooling readiness, PCBA process windows, mold flow assumptions, test fixtures, traceability, and supplier response discipline.
Global Industrial Matrix (GIM) addresses this challenge by benchmarking hardware across interconnected industrial pillars rather than in isolation. That matters when one program may involve HDI substrates, molded housings, harness routing, filtration interfaces, embedded sensing, and field durability requirements at the same time. In these environments, system-level visibility is not optional; it is the basis of reliable decision-making.
Where failures usually hide during early hardware development
Many teams focus on whether a supplier can make the part. Fewer ask whether the supplier can make the part under the exact process controls, documentation standards, and validation sequence the final product requires. That gap explains why a prototype can pass bench assembly and still fail pilot production, field deployment, or compliance review.
- Design-to-process mismatch: CAD and Gerber data may be complete, but DFM and DFA checks are not deep enough for repeatable mass production.
- Supplier capability mismatch: a factory may support prototype quantities of 10–50 units but lack stable controls for 500–2,000 unit pilot runs.
- Validation mismatch: electrical tests, leak tests, environmental tests, and mechanical checks may be run separately instead of as one acceptance logic.
- Documentation mismatch: version control, PPAP-style records, ECN flow, and inspection criteria are not synchronized across stakeholders.
Once these mismatches accumulate, teams often misread symptoms. They blame the molded part, the PCB, or the purchased connector, while the real issue is uncontrolled interaction between materials, tooling, assembly sequence, and acceptance thresholds.
Which prototype risk points matter most across electronics, mobility, agri-tech, and infrastructure?
In a comprehensive industrial environment, prototype risk is not uniform. A board-level electronics build may fail through solder voiding, warpage, or impedance drift. An automotive or mobility assembly may fail due to tolerance stack-up, thermal shock, or vibration fatigue. Smart agri-tech equipment often adds dust, moisture, and seasonal duty-cycle stress. Environmental infrastructure introduces long-duration exposure, maintenance access constraints, and stricter uptime expectations.
That is why benchmarking must compare process readiness across several dimensions at once. GIM’s value is the ability to connect semiconductor and electronics requirements with automotive discipline, tooling realism, industrial ESG expectations, and field-use operating conditions. This helps technical evaluators and commercial stakeholders avoid decisions made from a single-department viewpoint.
Before approving prototype spend, teams should review at least 5 key checkpoints: design maturity, supplier process control, tooling stability, compliance path, and field-condition fit. If even 1 of these remains weak, prototype success rates can drop sharply during the transition from engineering sample to pilot batch.
The table below summarizes common failure patterns by sector and shows why the “bad part” conclusion is often incomplete.
The pattern is consistent across industries: the visible defect appears at the part level, but the underlying cause is usually process integration. This is why procurement, engineering, and quality teams need a shared benchmark language before supplier nomination and tooling release.
Why cross-functional visibility reduces rework cost
A technical team may prioritize performance, while finance focuses on unit economics and project leaders focus on timing. All three are valid, but prototype failure usually occurs when these priorities are reviewed separately. A low quoted tool cost can hide unstable cycle time, weak cavity balance, or poor change-control discipline. A fast PCB turnaround can hide substitution risk in critical components.
GIM supports cross-functional review by aligning procurement criteria with technical benchmarks and operational risk indicators. That allows decision-makers to compare bids not only by piece price, but also by process capability, documentation maturity, standards alignment, and supply chain resilience across 3 stages: prototype, pilot, and scale-up.
How should buyers and engineering teams evaluate prototype suppliers before approval?
Supplier selection for prototypes should not be treated as a simplified version of production sourcing. In many cases, prototypes are where hidden supplier weaknesses first become visible. If buyers only compare quotation totals, they may miss the operational details that determine whether the first 20 units will lead smoothly to the next 200 or stall the program for 6–8 more weeks.
The most reliable evaluation model uses a balanced scorecard with at least 4 dimensions: engineering capability, process control, change management, and delivery reliability. For high-mix projects involving plastics, metal parts, PCBAs, cable assemblies, or filtration modules, this evaluation should also include sub-supplier coordination and test-readiness.
The table below provides a practical procurement framework for technical assessors, commercial reviewers, quality managers, and project owners who need to make defendable prototype sourcing decisions.
This framework helps different stakeholders ask the right questions. Operators care about assembly practicality. Quality teams care about repeatability. Finance cares about rework exposure. Executives care about launch risk. A structured supplier review connects these concerns instead of forcing each team to make separate assumptions.
A practical 4-step review before placing a prototype order
- Confirm technical baseline: freeze drawings, revision status, BOM critical items, and target acceptance criteria.
- Verify process route: check tooling status, PCBA line capability, secondary operations, inspection method, and packaging flow.
- Map risk ownership: define who signs off on substitutions, deviations, test failures, and corrective actions within 24–72 hours.
- Align commercial terms: confirm prototype quantity bands, sample cost logic, expected lead time, and pilot scale-up conditions.
When these 4 steps are documented before PO release, teams reduce avoidable confusion later. This is not bureaucracy. It is the shortest route to a more predictable prototype cycle.
What standards, process controls, and acceptance criteria should be aligned early?
Prototype work moves faster when standards are discussed before fabrication begins. In integrated manufacturing, relevant references may include ISO process controls, IATF-oriented automotive discipline, and IPC criteria for electronic assemblies. The point is not to overburden a prototype with full production paperwork, but to define which controls are essential from day one and which can mature in later phases.
For example, a plastic housing prototype may not need complete production automation, but it still needs stable dimensional control, clear resin traceability, and a documented response if shrinkage or warpage exceed agreed limits. A PCBA prototype may not require a full-scale validation lab, but it still needs soldering criteria, inspection logic, and revision traceability that can support root-cause analysis after functional testing.
Teams should usually define 6 acceptance items early: dimensional fit, electrical or functional verification, environmental exposure range, cosmetic threshold, traceability record, and deviation handling. Without these basics, every failed result becomes a debate instead of an actionable engineering conclusion.
GIM strengthens this process by translating standards into benchmarkable decision points across multiple sectors. That is useful when one supplier understands IPC language, another works closer to automotive quality methods, and a third comes from industrial equipment manufacturing. Shared interpretation reduces friction and shortens review cycles.
Common controls that should be specified before prototype build
- Material and component traceability for critical items, especially where alternate sourcing may appear during a 2–6 week build window.
- Inspection criteria with measurable thresholds, such as fit tolerance range, electrical pass/fail logic, and cosmetic acceptance level.
- Deviation approval path defining who can approve, reject, or quarantine parts if a process drifts or a substitution is proposed.
- Test sequence control so mechanical, environmental, and electrical evaluations do not invalidate one another by poor ordering.
Why this matters for finance and executive reviewers
Poorly defined prototype acceptance creates hidden commercial risk. A low initial quote may later generate expedited freight, repeated tooling edits, duplicated testing, and management time across several departments. In many industrial programs, these indirect costs exceed the original sample price difference. Standardized early controls make budget approval more credible because they reduce uncertainty, not just nominal unit cost.
How to reduce cost, delay, and rework without overspending on the first build
Teams often swing between two expensive extremes. One is under-controlling the prototype, which leads to rework, redesign, and schedule drift. The other is over-engineering the first build with production-level spending before core assumptions are validated. The right model is staged control: enough process discipline to generate trustworthy learning, without treating the first 10–30 units as a full launch.
A sensible cost strategy usually separates spending into 3 buckets: learning cost, risk-prevention cost, and scale-up cost. Learning cost covers early samples and DFM iterations. Risk-prevention cost covers fixture design, supplier audits, and benchmark reviews. Scale-up cost covers tooling optimization, documentation maturity, and logistics stabilization. When these buckets are mixed, programs either overspend too early or defer critical controls until failure appears.
For decision-makers, the useful question is not “What is the cheapest prototype?” but “Which prototype path gives reliable evidence for the next gate?” That may mean paying slightly more for traceability, fixture repeatability, or clearer documentation if it removes 1–2 rounds of avoidable rework later.
GIM supports this staged view by comparing hardware and supplier readiness across sectors and by highlighting where a cost-saving move is reasonable versus where it creates downstream risk. This is particularly valuable for distributors, sourcing teams, and project owners who must explain both technical and financial logic to multiple stakeholders.
Common misconceptions that increase prototype failure risk
“If the sample works once, the process is good enough.”
A single working unit proves possibility, not repeatability. Teams need a small but meaningful batch, often 10–30 units or another application-appropriate range, to understand variation and process stability.
“A lower tool quote always lowers project cost.”
Not necessarily. Lower upfront tooling may increase adjustment rounds, maintenance frequency, or dimensional variation. Total project cost should include timing, scrap risk, and validation repeat effort.
“Different sectors can use the same prototype logic.”
Only partly. Electronics, mobility hardware, smart agri-tech, and infrastructure modules share some methods, but their duty cycles, compliance expectations, and field failure modes are different. Cross-sector benchmarking is the safer approach.
Frequently asked questions before prototype sourcing and validation
The questions below reflect common concerns from engineers, buyers, quality personnel, project managers, distributors, and executives who need practical answers before approving hardware prototype work.
How long does a typical prototype cycle take?
It depends on complexity and supply chain exposure. A simpler fabricated part may move in 7–15 days, while integrated builds involving tooling, PCBA, and custom assemblies may require 3–8 weeks. The more important issue is whether the timeline includes DFM review, sample inspection, correction loop, and validation planning instead of only fabrication time.
What should buyers request from a prototype supplier besides a quotation?
Ask for process assumptions, revision control method, inspection plan, expected lead-time breakdown, critical material status, and deviation handling logic. If the supplier cannot explain these clearly, the quotation is incomplete no matter how attractive the unit price looks.
When is benchmarking more valuable than simply testing samples?
Benchmarking matters before and after testing. Before testing, it helps define what “good” should look like across process capability, standards, and operating context. After testing, it helps interpret whether a failure came from design, production control, material choice, or supplier execution. Without benchmarking, teams often react to symptoms instead of learning from them.
How do we know whether a prototype supplier can support scale-up later?
Review whether the supplier can demonstrate stable documentation, traceability, sub-supplier coordination, and process controls that can grow from prototype to pilot and then to higher-volume production. A prototype supplier does not need full production scale on day one, but the transition path should be visible and realistic.
Why work with GIM when prototype risk crosses multiple industries?
When programs combine electronics, mobility systems, smart agriculture, infrastructure hardware, and precision tooling, isolated evaluation is no longer enough. GIM provides a system-level benchmarking view that helps procurement officers, Tier-1 engineers, project leaders, quality managers, and business reviewers compare technical readiness and supply risk on the same decision framework.
This is especially useful when your team needs answers across several questions at once: whether a PCBA process is mature enough, whether a plastic injection mold factory can support the target tolerance window, whether supplier documentation aligns with ISO, IATF, or IPC expectations, and whether the proposed build path is commercially defensible for finance approval.
You can consult GIM for parameter confirmation, prototype supplier comparison, process benchmark review, lead-time assessment, standards alignment, sample planning, and cross-sector risk identification. That support is designed for real purchasing and engineering decisions, not abstract analysis.
If your hardware prototype is facing repeated test failures, unclear root causes, uncertain supplier capability, or growing rework cost, the right next step is to review the full system behind the part. Contact GIM to discuss technical selection, delivery timing, compliance expectations, sample support, custom benchmarking scope, or quotation alignment before the next build locks in avoidable risk.
- electronics
- tech hardware
- PCBA manufacturing
- Mobility
- Agri-Tech
- crop monitoring
- Industrial ESG
- industrial sustainability
- tooling solutions
- plastic injection mold factory
- HDI substrates
- Precision tooling
- Smart Agri-Tech
- Global manufacturing
- Modern manufacturing
- Engineering standards
- Tier-1 engineers
- Industrial infrastructure
- Environmental infrastructure
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.