Monday, May 22, 2024
Printed Circuit Board Assembly Problems Linked to Solder Paste
by
Published
Views:
In electronics manufacturing, printed circuit board assembly issues linked to solder paste can quietly undermine PC hardware reliability, quality control, and operational efficiency. For technical evaluators, project leaders, and business decision-makers navigating Green Mobility, energy management, precision machining, precision farming, smart irrigation, and advanced suspension systems, understanding these defects is essential to reducing risk, improving process stability, and strengthening cross-industry production performance.
In practical terms, most solder paste-related PCB assembly problems are not isolated shop-floor nuisances. They are early warnings of larger issues in process control, supplier consistency, stencil design, storage discipline, and inspection strategy. If these weaknesses are missed, the result is not just rework. It can mean field failures, warranty exposure, delayed launches, unstable throughput, and weak confidence in manufacturing partners.
For most readers searching this topic, the key question is simple: which solder paste problems matter most, how do they show up during assembly, and how can teams prevent them before they damage quality or cost performance? The short answer is that defects such as insufficient solder, bridging, voiding, tombstoning, solder beads, and non-wet opens are usually tied to a combination of paste chemistry, handling conditions, print process setup, component design, and reflow control. The most effective response is not a single fix, but a disciplined process window built around material selection, print consistency, inspection, and root-cause validation.
Which PCB assembly problems are most often linked to solder paste?
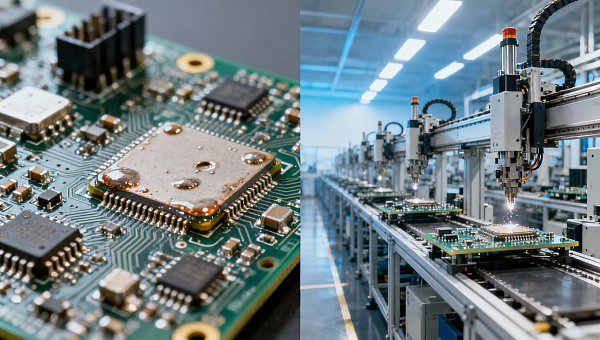
When manufacturers investigate printed circuit board assembly defects, solder paste is often one of the first variables that deserves scrutiny. It affects deposition volume, wetting behavior, joint formation, and ultimately long-term reliability. The most common solder paste-related defects include:
- Insufficient solder: Too little deposited paste can produce weak joints, opens, or intermittent electrical behavior.
- Solder bridging: Excess paste, poor stencil design, or slump can create shorts between adjacent pads.
- Tombstoning: Small passive components lift on one side due to imbalanced wetting forces.
- Voiding: Entrapped gases or volatile residues create internal cavities in solder joints, especially relevant in thermal or power electronics.
- Solder balling and beads: Small solder particles separate during reflow and can create contamination or latent reliability concerns.
- Head-in-pillow and non-wet opens: Often seen in area-array devices or challenging surface finishes where solder fails to coalesce properly.
- Misalignment and poor joint geometry: Uneven print release or paste spread can compromise component placement and final solder shape.
These defects matter differently depending on the application. In consumer electronics, they may drive cosmetic rejects or short-term failures. In automotive controls, power modules, irrigation controllers, industrial sensor platforms, or motion systems, the same defects can create serious durability and safety risks. That is why solder paste should be treated as a strategic quality variable, not just a consumable.
Why solder paste causes failures even when the rest of the assembly line looks normal
A common misconception is that if placement equipment, ovens, and inspection tools are functioning, then solder paste should not be the root cause. In reality, solder paste sits at the intersection of material science and process execution. Even a well-equipped line can produce unstable outcomes if paste behavior is inconsistent.
The main failure drivers usually fall into five categories:
- Paste formulation mismatch: Flux activity, alloy type, powder size, and viscosity must suit the pad geometry, component package, and thermal profile.
- Storage and handling errors: Improper refrigeration, uncontrolled warm-up time, expired shelf life, or excessive re-mixing can change printability and wetting behavior.
- Stencil and aperture design issues: Poor area ratios, improper thickness, or aperture shapes can prevent accurate paste transfer.
- Printing process instability: Squeegee pressure, print speed, separation speed, under-stencil cleaning frequency, and board support affect deposit consistency.
- Reflow profile incompatibility: If the heating profile does not align with paste chemistry and board mass, defects such as voiding, beads, and non-wet opens become more likely.
For technical and commercial evaluators, this means a defect should rarely be blamed on “bad paste” alone. The more useful question is whether the paste-process-package combination is robust enough for the target product and production environment.
How to identify whether solder paste is really the root cause
Teams often lose time because they react to visible defects without isolating the actual source. Effective diagnosis requires a structured approach rather than assumptions.
Start with the print itself. Solder paste inspection data can reveal whether the problem begins at deposition. Look for recurring volume variation, poor height control, edge deformation, offset, or incomplete aperture release. If printing is unstable, downstream defects are often just symptoms.
Next, compare defect patterns by:
- Component type and package size
- Board location and thermal mass
- Stencil aperture group
- Time since paste thawing or loading
- Lot number, supplier batch, and storage history
- Reflow zone behavior and temperature uniformity
If defects correlate strongly with one paste lot, one print interval, one package family, or one thermal region of the board, the investigation becomes much more actionable.
For higher-value products, root-cause confirmation should also include:
- SPI trend review for deposition variation over time
- AOI and AXI correlation to connect print quality with solder joint outcomes
- Cross-section analysis for voiding, wetting, and intermetallic behavior
- Reflow profile verification on populated production boards, not just test coupons
- Material traceability review covering storage, open time, and change records
This evidence-based method helps quality managers, project leads, and procurement teams distinguish between controllable process drift and deeper supplier or design issues.
What process controls reduce solder paste-related defects the most?
If the goal is to reduce scrap, improve first-pass yield, and protect product reliability, a few controls typically deliver the highest return.
1. Match solder paste to the actual assembly challenge
Not every paste suits fine-pitch devices, bottom termination components, power electronics, or mixed-technology boards. Selection should account for alloy system, particle size, flux chemistry, stencil thickness, finish compatibility, and reliability demands. For example, high-density electronics may require tighter print resolution, while thermally demanding assemblies may prioritize void reduction and joint durability.
2. Tighten storage and usage discipline
Many defects begin before printing starts. Standardize refrigerated storage, thawing times, humidity control, open-life limits, and lot rotation. If operators handle paste differently by shift or line, print consistency usually suffers.
3. Optimize stencil design instead of compensating at the machine
When print problems are chronic, repeated machine parameter changes are rarely the best long-term answer. Aperture reductions, home-plate designs, step stencils, nano-coatings, and thickness adjustments often solve the root issue more effectively.
4. Use SPI as a process control tool, not just a screening tool
Many factories collect solder paste inspection data but do not use it to manage drift. Trend analysis can expose gradual changes in transfer efficiency, board support, cleanliness, or paste condition before visible assembly failures rise.
5. Validate the reflow profile against real product conditions
Board density, copper balance, large thermal components, and enclosure-driven design constraints all affect actual reflow performance. Profile recipes must be validated under production-representative loads.
For operations leaders, these controls matter because they reduce the hidden cost stack of rework labor, schedule disruption, line stoppages, excess inspection, and customer return exposure.
How different stakeholders should evaluate solder paste risk
Because the audience for this topic spans technical, operational, and business roles, evaluation criteria should be role-specific.
For engineers and technical evaluators
- Check print process capability, SPI repeatability, and reflow margin.
- Assess compatibility with component miniaturization, thermal mass variation, and surface finish.
- Review defect pareto trends by package family and board design region.
For quality and safety managers
- Focus on defect escape risk, latent reliability concerns, traceability, and corrective action discipline.
- Prioritize evidence of stable control plans rather than one-time trial success.
For project managers and manufacturing leaders
- Look at first-pass yield, rework rate, line utilization, and process repeatability across shifts and sites.
- Confirm whether the paste strategy supports ramp-up speed and engineering change resilience.
For procurement, commercial evaluators, and decision-makers
- Evaluate total cost of ownership, not only unit paste price.
- Ask whether lower-priced materials increase defects, downtime, validation effort, or customer risk.
- Review supplier support capability, batch consistency, documentation quality, and standards alignment.
This broader lens is especially important in cross-sector manufacturing environments where electronics assemblies support mobility platforms, industrial controls, agricultural automation, filtration systems, and connected infrastructure. A solder paste decision that looks economical in purchasing can become expensive in warranty, service, and field reliability.
What to ask a PCB assembly supplier or internal factory before approving production
Whether you are qualifying a contract manufacturer, auditing an internal line, or benchmarking suppliers, the right questions can quickly reveal process maturity.
- What solder paste types are approved for this product class, and why?
- How are storage, thawing, open time, and lot traceability controlled?
- What SPI acceptance thresholds are used, and how are trends reviewed?
- How often is stencil cleaning performed, and what triggers adjustments?
- How is the reflow profile validated for high-mix or thermally uneven boards?
- What are the top recurring solder-related defects, and what corrective actions reduced them?
- How is process performance benchmarked to IPC, ISO, IATF, or customer-specific requirements?
Strong answers should be specific, data-backed, and repeatable. Vague assurances such as “we rarely have issues” are far less useful than measured evidence showing defect trends, control limits, and successful corrective action histories.
When solder paste problems signal a larger manufacturing weakness
Recurring PCB assembly problems linked to solder paste often indicate one of three broader weaknesses: poor process discipline, weak engineering-to-production transfer, or inadequate supplier qualification. If the same defect families persist despite line adjustments, the issue may involve design for manufacturability, unrealistic takt expectations, inconsistent operator methods, or fragmented quality ownership.
In that sense, solder paste defects are valuable signals. They show where a production system lacks robustness. Organizations that treat them as strategic indicators tend to improve not only assembly quality, but also launch confidence, cross-site standardization, and customer trust.
This is particularly relevant for advanced manufacturing ecosystems where electronics are embedded into larger industrial systems. In EV subsystems, smart farming equipment, fluid management controls, robotics, and sensor-based infrastructure, electronic assembly defects can cascade into mechanical downtime, software faults, or certification delays. That makes early control of solder paste-related issues a business priority, not merely a process detail.
Conclusion: focus on process stability, not isolated fixes
Printed circuit board assembly problems linked to solder paste are rarely random. They usually result from a mismatch between material properties, stencil strategy, printing discipline, component design, and thermal processing. The fastest way to reduce risk is to stop treating solder paste as a standalone consumable and start managing it as a core process variable with measurable impact on yield, reliability, cost, and production resilience.
For technical teams, that means using inspection data and root-cause analysis to separate symptom from source. For business and project stakeholders, it means evaluating total operational impact rather than material price alone. And for quality-driven organizations, it means building a repeatable control window that protects performance across products, lines, and sectors.
When that approach is in place, solder paste stops being a hidden source of defects and becomes part of a stable, high-confidence PCB assembly strategy.
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.