Monday, May 22, 2024
Electronics Manufacturing Costs Hidden in Yield Loss
by
Published
Views:
In electronics manufacturing, hidden costs rarely come from materials alone—they often stem from yield loss across printed circuit board assembly, PC hardware integration, and precision machining workflows. For teams focused on Operational efficiency, understanding how defects, process drift, and quality gaps erode margins is essential to making smarter decisions across supply chains, energy management, and advanced industrial systems.
Why yield loss quietly becomes one of the largest electronics manufacturing costs
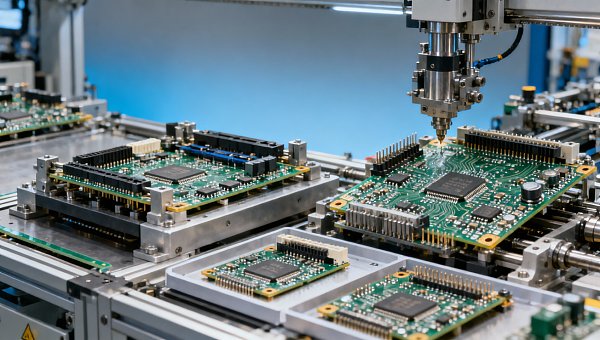
Many procurement teams still evaluate electronics manufacturing costs through visible line items such as copper, laminates, semiconductors, labor, freight, and tooling. That view is incomplete. In real production environments, yield loss often becomes the hidden cost multiplier because one defective board, one unstable process window, or one repeated test failure can trigger scrap, rework, retesting, delayed shipment, and excess inventory at the same time.
For PCBA, a seemingly small first-pass yield drop from 98% to 94% can materially change cost per good unit when volumes move from prototype lots into medium or high-volume runs. The same pattern appears in system integration and precision machining. A failed connector alignment, thermal interface error, or tolerance mismatch within ±0.05 mm to ±0.10 mm may not look dramatic on paper, yet it can consume hours of engineering review and multiple production cycles.
This matters across industries, not only in consumer electronics. Automotive control modules, smart agri-tech devices, industrial filtration controllers, EV subsystems, and infrastructure monitoring hardware all depend on stable yield. When cross-sector programs share components, test methods, or suppliers, the financial impact of poor yield spreads beyond one product line and starts affecting planning, warranty exposure, and cash flow.
Global Industrial Matrix (GIM) addresses this issue by benchmarking hardware and process risks across Semiconductor & Electronics, Automotive & Mobility, Smart Agri-Tech, Industrial ESG & Infrastructure, and Precision Tooling. For decision-makers, that cross-sector visibility is important because yield loss is rarely a single-factory problem. It is usually a system-level problem involving design rules, supplier capability, process control, compliance expectations, and field-use conditions.
What hidden cost layers are usually missed?
A practical cost review should separate direct manufacturing loss from downstream business loss. Direct loss includes scrap boards, replacement components, extra solder paste usage, repeated AOI or ICT cycles, and operator time. Downstream loss includes delayed customer approval, line rescheduling, missed delivery windows of 7–15 days, and financial holdbacks caused by unstable quality performance.
- Rework cost: labor, fixtures, retest time, and the risk of latent reliability issues after repair.
- Planning cost: schedule disruption, partial lot release, and excess safety stock held to protect delivery.
- Quality cost: more frequent inspections, additional sample validation, and corrective action documentation.
- Commercial cost: debit claims, price pressure in future negotiations, and reduced trust from OEM or distributor channels.
For finance approvers, the key lesson is simple: yield loss should not be treated as a narrow shop-floor KPI. It is a cost leakage mechanism with effects on gross margin, working capital, and supplier risk exposure. For project managers, it becomes a delivery risk. For quality leaders, it becomes a compliance and traceability issue. For operators, it often shows up first as unstable setup conditions or recurring defect patterns.
Where do hidden yield losses usually start in multi-step manufacturing?
In complex industrial manufacturing, yield loss often begins before assembly. It may start in design-for-manufacturability gaps, supplier material variability, inadequate incoming inspection criteria, or mismatched tolerances between electronic and mechanical parts. Once a product passes through 3 to 5 major stages such as SMT, through-hole assembly, system integration, test, and pack-out, the cumulative cost of one upstream mistake rises sharply.
For electronics programs that combine HDI substrates, machined housings, connectors, sensors, and power modules, each interface becomes a risk point. A board can pass electrical test but still fail in final assembly because standoff height, torque sequence, enclosure flatness, or cable routing creates stress. That means reported yield at one station may look acceptable while total factory yield remains weak.
The table below shows how hidden yield loss typically develops across common production stages. It is especially useful for technical evaluators and sourcing teams comparing suppliers with different process maturity levels.
The table highlights an important procurement insight: low quoted unit price does not always mean low electronics manufacturing costs. If the supplier cannot control variation across stages, cost reappears later as rework, warranty risk, or poor delivery reliability. GIM helps teams compare these failure paths in a structured way instead of relying only on price sheets.
Three early warning signals that should not be ignored
Most hidden cost problems leave signals before they become severe. The challenge is that organizations often review them separately. Procurement sees lead-time drift, quality sees defect recurrence, and engineering sees test instability, but nobody combines the information into one cost-risk picture.
- Recurring defects across 2–3 lots, even if each lot still ships after rework. This indicates process instability rather than isolated error.
- Inspection intensity keeps increasing every month or quarter. More checks may protect outgoing quality, but they also hide underlying yield weakness.
- Supplier response focuses only on containment, not on parameter control, capability evidence, or root-cause closure.
When these signals appear, business evaluators should request process capability details, control plans, defect pareto trends, and recovery timelines. In multi-sector manufacturing, that discipline matters because a supplier suitable for one product category may not be mature enough for another with tighter reliability, thermal, or compliance requirements.
How should buyers and engineers evaluate suppliers beyond unit price?
A reliable sourcing decision requires more than comparing quotations. Technical teams, commercial reviewers, and finance approvers need a shared framework that connects manufacturing yield to lifecycle cost. In practice, 5 core dimensions are usually more useful than a long checklist: process control, inspection coverage, change management, standards alignment, and responsiveness during corrective action.
For electronics manufacturing costs, the most common mistake is to compare suppliers only on quoted assembly rates while ignoring the cost of non-conformance. A supplier with lower visible pricing but weaker control over stencil life, MSL handling, torque management, calibration intervals, or traceability records may create higher total cost within 2–4 production cycles.
The next table can be used by procurement managers, quality specialists, and engineering project owners during RFQ review, pilot approval, or supplier requalification. It focuses on practical assessment points rather than marketing claims.
This comparison supports better total-cost decisions. It also helps distributors and channel partners who need to explain why one manufacturing source is safer than another for industrial buyers. The right supplier is not just the one that can build a product once; it is the one that can repeat acceptable yield under real delivery pressure.
A practical 4-step review before approval
When internal teams are under time pressure, a short review sequence works better than a broad but shallow audit. For prototype, NPI, or transfer projects, the following 4-step method is often enough to expose hidden yield risk early.
- Step 1: Confirm critical-to-quality points, including component sensitivity, thermal limits, connector cycles, tolerance interfaces, and inspection criteria.
- Step 2: Review pilot yield, rework categories, and failure pareto from at least 1–2 representative builds rather than one engineering sample.
- Step 3: Verify standards usage such as relevant ISO, IATF, or IPC frameworks where the application demands it.
- Step 4: Define recovery actions, response windows, and ownership if yield drops after launch.
GIM adds value here by translating cross-industry benchmarking into decision support. That is particularly useful when teams source mixed systems that blend electronics, mobility hardware, environmental modules, and precision-machined components under one procurement program.
Which standards, controls, and operating practices reduce yield-driven cost leakage?
Hidden cost reduction is not achieved through inspection alone. It depends on disciplined operating controls supported by appropriate standards. In electronics and adjacent industrial sectors, teams often reference ISO quality frameworks, IATF requirements for automotive-linked programs, and IPC workmanship or acceptability criteria for PCB-related processes. The goal is not paperwork. The goal is stable execution and clearer acceptance boundaries.
For operators and quality managers, daily controls matter more than broad statements. Examples include baking and moisture handling for sensitive devices, solder paste exposure timing, tool calibration intervals, ESD discipline, torque verification, fixture validation, and documented response to recurring defects. Even a 15–30 minute drift in handling practice can affect defect rates when products use fine-pitch packages or thermally sensitive materials.
For project leaders, it is also important to align control depth with application criticality. A consumer accessory, an EV subsystem, and an environmental monitoring controller should not all be governed by the same risk assumptions. As product criticality increases, incoming control, traceability depth, and process validation requirements usually increase as well.
Control areas that usually pay back fastest
1. Design-to-process alignment
When pad design, stack-up, enclosure geometry, and assembly access are reviewed before production transfer, many high-cost defects can be prevented rather than repaired. This is especially important for compact assemblies with dense layouts, high-current paths, or mixed electronic-mechanical interfaces.
2. Controlled change implementation
A small revision change in firmware, fixture, adhesive, or surface finish can affect yield. Effective sites define revision release timing, line-side document updates, and sample approval gates. Without that discipline, factories may mix old and new conditions for several shifts.
3. Closed-loop defect analysis
Not every defect needs a major investigation, but repeat defects do. If the same issue appears over 2 consecutive lots or more than one process step, teams should move from sorting to root-cause containment. That reduces the chance of carrying hidden failures into field use.
In a cross-sector environment, GIM’s benchmarking approach helps companies decide where to apply tighter controls and where simpler controls are enough. That balance matters for budget holders who need to reduce cost leakage without over-engineering every process.
Common misconceptions, cost trade-offs, and what decision-makers should do next
One common misconception is that rework is cheaper than prevention. In low volumes, that may appear true for a short period. But once a product moves into repeated shipments, rework adds labor, handling risk, and reliability uncertainty. Another misconception is that final test can protect the business from weak upstream control. In reality, final test often detects symptoms, not causes, and it cannot fully screen latent mechanical or thermal weaknesses.
There is also a trade-off between aggressive cost-down sourcing and process resilience. A lower-cost supplier may still be the right choice if capability, standards alignment, and corrective-action discipline are proven. The issue is not whether a quote is low. The issue is whether the total manufacturing model remains stable over 3, 6, or 12 months of delivery.
For organizations managing electronics manufacturing costs across multiple product families, the smartest move is to treat yield analysis as part of sourcing governance. Link technical data, supplier performance, and commercial exposure in one review process. That is where GIM is particularly relevant: it connects benchmarks across electronics, mobility, agriculture, infrastructure, and precision tooling so that decisions reflect real industrial complexity rather than siloed assumptions.
FAQ: the questions buyers and engineers ask most often
How can we estimate the cost impact of yield loss before mass production?
Start with pilot builds, not just engineering samples. Review first-pass yield, rework hours, top defect categories, and expected lot sizes. Then compare the cost of one additional inspection layer versus the cost of recurring rework over the first 2–4 production cycles. Even simple scenario planning can reveal whether the quoted unit price is hiding downstream cost exposure.
What are the most important documents to request during supplier evaluation?
Ask for process flow, control plan, defect pareto, traceability method, calibration records for key tools, and evidence of standards use relevant to the application. For assemblies that combine electronics and mechanical parts, also review tolerance control, torque instructions, and revision management practice.
Which scenarios are most vulnerable to hidden yield loss?
NPI transfers, dual-sourcing programs, tight-package-density assemblies, mixed-material products, and applications with harsh thermal or vibration exposure are all vulnerable. These programs often fail not because of one major defect, but because several minor variabilities combine across the process chain.
How long does it usually take to identify the main yield-loss drivers?
For a focused review with available production records, an initial diagnosis can often be developed within 1–2 weeks. Deeper verification may take longer if multiple suppliers, tooling interfaces, or standards-related acceptance questions are involved. The key is having comparable data from materials, assembly, test, and field feedback.
Why work with GIM
GIM is built for teams that need more than a narrow component view. We provide cross-sector technical benchmarking that helps procurement officers, Tier-1 engineers, quality leaders, and industrial strategists understand where hidden cost is really coming from and how it affects operational efficiency. Our perspective spans Semiconductor & Electronics, Automotive & Mobility, Smart Agri-Tech, Industrial ESG & Infrastructure, and Precision Tooling.
If you are reviewing electronics manufacturing costs affected by yield loss, you can contact GIM for support on parameter confirmation, supplier comparison, process-risk mapping, standards alignment, delivery-cycle assessment, sample evaluation logic, and quotation discussions tied to total cost rather than price alone.
This is especially useful when your team needs to evaluate PCB assembly stability, hardware integration risk, machining tolerance interactions, or cross-industry sourcing options under one project. A structured discussion now can help reduce scrap, prevent repeated rework, and improve decision quality before cost leakage becomes permanent.
- electronics
- semiconductors
- printed circuit board assembly
- electronics manufacturing
- Mobility
- sensors
- Agri-Tech
- Industrial ESG
- industrial filtration
- energy management
- precision machining
- PC hardware
- HDI substrates
- Precision tooling
- Technical benchmarking
- Smart Agri-Tech
- Operational efficiency
- Tier-1 engineers
- Industrial strategists
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.