Monday, May 22, 2024
CNC Verification: Which Measurements Prove Machined Part Conformance?
by
Published
Views:
CNC Verification: Which Measurements Prove Machined Part Conformance?
A machined part can look correct, fit through a quick bench check, and still fail the conditions that matter in service. A bore may be the right diameter but mislocated relative to its datum structure. A shaft may meet size limits yet have excessive runout. A sealing face may be flat enough for a basic gauge but too rough, damaged, or distorted to maintain a reliable seal.
That is why CNC verification is more than dimensional inspection. Often written as cnc-verifiering in cross-border technical documentation, it is the disciplined process of converting inspection results into defensible evidence that a machined part conforms to the drawing, the applicable standard, and the intended functional requirement. For quality and safety teams, the key question is not simply, “Was it measured?” It is, “Did the measurement method prove the feature that controls risk?”
The answer depends on the part. An EV drivetrain housing, a semiconductor equipment bracket, an autonomous agricultural actuator body, and a membrane-filtration manifold all present different failure paths. Yet the verification logic is consistent: establish the correct requirement, control the measurement system, inspect the characteristics that affect function, and preserve records that can be reviewed later without relying on memory or assumption.
A drawing is the starting point, not the whole verification plan
Part drawings define nominal dimensions, tolerances, datum references, material notes, finishes, threads, coatings, and often special process requirements. They do not automatically tell an inspection team how to sequence every measurement or how much inspection is needed at each production stage. That must be developed in a control plan or inspection plan that connects engineering intent to practical measurement.
A useful plan separates features into three groups. The first includes critical-to-function characteristics: interfaces that control fit, load transfer, pressure retention, alignment, electrical clearance, or motion. The second includes features that influence assembly efficiency or durability. The third covers general workmanship and lower-risk dimensions. Treating every drawing dimension as equally important consumes inspection capacity while obscuring the few characteristics most likely to create safety, reliability, or containment problems.
This prioritization should be approved by the responsible engineering and quality functions. An inspector should not independently decide that a geometric tolerance is “less important” because a part seems likely to assemble. A feature’s importance is determined by design intent, not by how easy it is to measure.
The measurements that usually establish conformance
No universal checklist can prove every machined part conforming, but several measurement categories repeatedly determine whether evidence is complete. The right mix should trace directly back to the released drawing and any customer-specific requirements.
Size is still the foundation. Calipers, micrometers, bore gauges, height gauges, pin gauges, thread gauges, and air gauges can provide efficient measurements when they are capable for the tolerance and applied correctly. The common error is assuming that one convenient reading represents a whole feature. A turned diameter may need readings at more than one axial location and angular position if taper, lobing, or out-of-roundness is relevant. A milled pocket may require width, depth, corner condition, and position relative to functional datums rather than one nominal check.
Feature size and feature geometry are not interchangeable. A hole can accept a plug gauge while still failing positional tolerance. A flat face can pass a height measurement at selected points while exceeding flatness. Where the drawing uses geometric dimensioning and tolerancing, verification must reproduce the datum scheme and tolerance definition. ISO 1101 and ASME Y14.5 are widely used frameworks for geometrical tolerancing, but they should not be treated as interchangeable by default; the governing drawing convention, revision, and contractual requirements must be clear.
Why datum simulation decides whether a geometric result is credible
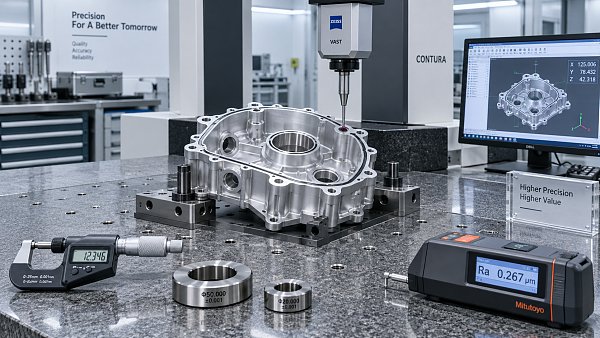
Many disputes over CNC part acceptance arise from datum setup rather than machining. If a drawing identifies a primary mounting face, a secondary bore, and a tertiary edge, the inspection fixture or CMM alignment must simulate those datums in a way that reflects the stated design intent. Aligning the part to whichever surfaces produce the most favorable result is not verification.
Coordinate measuring machines are especially valuable for complex profiles, patterns of holes, true position, perpendicularity, concentricity-related requirements, and freeform surfaces. Their output is only as reliable as the program, probes, stylus qualification, workholding, thermal condition, filtering choices, and datum construction. A CMM report with many decimal places can create false confidence if these conditions are not understood.
Functional gauges can be stronger evidence than a long coordinate report when they directly test the assembly condition. A dedicated go/no-go gauge, for example, may efficiently verify whether a pattern of features accepts its mating component under defined conditions. But a functional gauge must itself be controlled: its acceptance criteria, wear limits, calibration status, and relationship to the drawing need documented justification. It is not a substitute for understanding the requirement; it is a method selected to prove it.
Surface finish, edges, and threads are often under-verified
Surface texture requirements are frequently written as a roughness value, commonly expressed through parameters such as Ra. That value matters, but it is not the complete story. Measurement direction, cutoff selection, instrument condition, surface lay, and the actual function of the interface all affect interpretation. A sealing land, sliding surface, adhesive bond area, or hygienic fluid-contact channel may require closer attention than a general external face with the same nominal roughness callout.
Visual inspection also has a legitimate role, provided criteria are defined. Burrs, sharp edges, tool marks, dents, embedded contamination, incomplete deburring, and handling damage can create safety or service risks that dimensional instruments do not capture. “No sharp edges” is too vague unless the drawing, workmanship standard, or internal acceptance criterion explains what is acceptable and how it is assessed.
Threads deserve the same discipline. A thread’s apparent major diameter does not prove pitch, flank form, functional engagement, or damage-free condition. Appropriate thread gauges and visual examination may be required, while critical threaded joints may also call for verification of depth, counterbore geometry, thread relief, or mating-part engagement. The drawing and applicable thread standard govern the method; improvised checks invite inconsistent decisions.
Measurement-system capability is part of the evidence
A reported value cannot prove conformance if the measurement system is unable to distinguish acceptable from unacceptable product with sufficient confidence. Resolution alone is not capability. Sources of variation include instrument bias, repeatability, reproducibility between operators, fixture effects, part temperature, surface condition, measurement force, software settings, and calibration condition.
This becomes acute when tolerances are tight or the feature is difficult to access. A caliper may be suitable for a broad external dimension but unsuitable for a narrow tolerance on a bore or a datum-dependent location. Likewise, a calibrated instrument is not automatically suitable for every application. Calibration confirms a controlled state against known references; it does not establish that the chosen method has adequate uncertainty for the part characteristic.
Quality systems commonly use measurement system analysis, including gauge repeatability and reproducibility studies, to examine whether a method is fit for purpose. The study design should reflect the actual inspection process: representative parts, expected operators, real fixturing, and the normal measurement environment. Where a formal study is not practical, the organization should still document why the method is adequate and how uncertainty is considered at the acceptance boundary.
Traceability turns inspection into an auditable record
For a safety-relevant or customer-controlled component, the inspection report should allow a reviewer to answer basic questions months later: Which drawing revision applied? Which part and production lot were inspected? Who performed the check? Which instrument or CMM program was used? Was it within its calibration interval? What was measured, against what tolerance, and what was the result?
Material documentation must follow the same chain. A dimensional report does not prove that the specified alloy, polymer grade, heat treatment, plating, or passivation condition was used. Depending on the requirement, traceability may involve material certificates, incoming-lot identification, process records, subcontractor documentation, and part marking or batch controls. The appropriate level depends on the product’s criticality and contractual requirements, but broken traceability makes a focused containment action much harder.
Sampling plans also require care. Sampling can be appropriate for stable, capable processes and lower-risk characteristics, but it does not make a critical feature safe by itself. Where one nonconforming feature could create a severe assembly, pressure, motion, electrical, or personnel hazard, organizations often need stronger prevention and detection controls than a routine sample check. The correct approach should be established through risk analysis, process capability evidence, and customer or regulatory obligations where applicable.
A practical review before approving a machined part
Before release, quality and safety personnel should look beyond a pass/fail column. Confirm that the inspection report matches the correct drawing revision; critical dimensions and GD&T characteristics were measured from the intended datums; the selected tools or programs are appropriate for the tolerances; surface, thread, edge, and cleanliness requirements were not silently skipped; and material and process records remain connected to the inspected lot.
It is equally important to review exceptions. A rework, deviation, concession, altered inspection method, or substituted material should never disappear inside a generic “accepted” status. These conditions need formal disposition by the authority defined in the quality system and, where required, customer approval.
Global Industrial Matrix approaches this problem as a cross-sector benchmarking issue rather than a tooling-only question. The evidence expected for precision-machined hardware is shaped by the interfaces it serves: automotive mobility systems, electronics equipment, agricultural machinery, and environmental infrastructure each connect machining quality to broader reliability and supply-chain exposure. Comparing documentation practices against applicable ISO, IATF, IPC, and project-specific requirements helps procurement and engineering teams identify where an apparently complete inspection package is actually incomplete.
The strongest CNC verification package is not necessarily the longest one. It is the one in which every critical claim can be traced to a requirement, a capable measurement method, a controlled record, and a clearly identified production lot. That standard of proof makes nonconformance easier to contain, supplier discussions more factual, and downstream safety decisions less dependent on assumption.
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.