Monday, May 22, 2024

What limits achievable tolerances in micro precision machining?
by
Published
Views:
What limits achievable tolerances in micro precision machining?
A machine’s positioning resolution is not the same as its ability to hold part tolerances. In micro precision machining, achievable accuracy depends on the interaction of thermal drift, tool runout and wear, material microstructure, cutting forces, and measurement uncertainty. The practical challenge is determining which constraint dominates under actual production conditions—not simply comparing nominal equipment specifications.
There is no universal minimum tolerance for the process. A shallow pocket in a rigid workpiece and a deep microbore in a thin-walled component may require entirely different capability assessments, even on the same machine. A credible tolerance claim must identify the feature, material, inspection method, and production conditions behind it.
Start with the feature requirement, not the machine brochure
“Micron accuracy” is incomplete without a definition. Does it describe positioning accuracy, repeatability, bore diameter, profile, or location relative to a datum? A machine can return consistently to one commanded position while retaining a systematic positioning error. Likewise, a bore may meet its diameter requirement but fail cylindricity or positional tolerance.
ISO 230-2 provides methods for evaluating the positioning accuracy and repeatability of numerically controlled axes. Those results are useful machine-level evidence, but they do not establish finished-part capability. Cutting introduces additional influences: tool deflection, spindle behavior at operating speed, workholding distortion, and material response.
Before comparing suppliers, define what is actually being accepted. A hole’s measured size can depend on sampling depth, filtering, and the association method used to calculate its geometry. If the drawing, inspection program, and supplier quotation imply different definitions, disagreement is built into the project before machining starts.
Thermal stability often sets the production limit
Heat changes the relationship between the cutting edge and the workpiece. Spindle bearings warm up, machine structures expand unevenly, coolant temperature changes, and the part itself moves with temperature. Uniform expansion is relatively straightforward to estimate; temperature gradients can also cause bending and angular error.
For scale, a 100 mm length with a thermal expansion coefficient of 10 micrometers per meter per kelvin changes by approximately 1 micrometer for a 1 K temperature change. This is an illustrative calculation, not a material specification. Even when the machined feature is tiny, the machine structure and fixture locating it may span much larger distances.
ISO 1 establishes 20 °C as the standard reference temperature for geometrical and dimensional properties. That does not mean every operation must occur at exactly 20 °C. It means temperature, compensation, and stabilization conditions must support a defensible comparison with the specified dimensions.
A useful qualification run includes startup, sustained cutting, and interruptions representative of production. A short trial after careful warm-up may miss drift following a tool change, coolant shutdown, or overnight stop. The important question is whether the process stays within its error allowance throughout the intended operating cycle.
The cutting edge does not behave like a scaled-down conventional tool
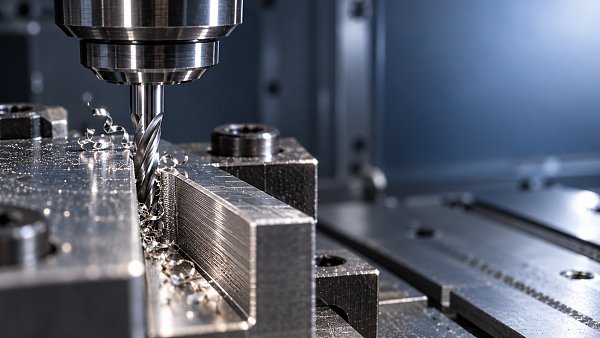
As tool diameter decreases, runout and cutting-edge radius become large relative to the intended chip thickness. One flute may carry most of the load while another contributes little cutting. The resulting imbalance affects feature size, surface texture, tool life, and the likelihood of breakage.
Runout measured at the holder is therefore insufficient on its own. What matters is the effective cutting-edge motion near the tool tip, with the actual tool assembly and relevant operating conditions. Excessive overhang makes the situation worse by reducing stiffness and increasing sensitivity to vibration.
Reducing feed is not an unlimited route to better accuracy. When undeformed chip thickness becomes too small relative to the edge radius, cutting can shift toward rubbing and ploughing. Forces become less predictable, burr formation may increase, and the surface may recover elastically behind the edge. The transition depends on the tool, material, friction, and cutting conditions; no single threshold applies universally.
This is why a nominally light finishing pass can underperform a more deliberate cut. The process needs enough engagement to form a stable chip without creating excessive deflection. Tool wear gradually changes that balance, so the qualified tool-life window matters as much as the first acceptable component.
Geometry determines how much cutting error becomes dimensional error
A deep narrow slot is constrained by tool reach, chip evacuation, and sidewall deflection. A thin rib adds workpiece flexibility. A blind microbore introduces access and inspection difficulties that an open surface does not have. These features should not inherit a tolerance promise established on a shallow test pocket.
Tool deflection also varies through the path. Engagement changes at corners and during entry, so a single diameter compensation cannot necessarily correct the entire profile. Repeated finishing passes may reduce remaining stock, but they also add cycle time and exposure to wear or rubbing. Their value should be demonstrated on the critical geometry.
Material and workholding create limits that compensation cannot always remove
At small feature scales, local material structure becomes more visible in the machining response. Grain orientation, hard particles, inclusions, and phase boundaries can change forces and surface formation over short distances. A material grade alone may not adequately describe machinability when the feature size approaches relevant microstructural dimensions.
Soft, ductile materials may smear or develop burrs that obscure the intended edge. Hard or abrasive materials may accelerate edge wear or produce localized damage. Material condition, heat treatment, and stock consistency therefore belong in the qualification record, rather than being treated as purchasing details.
Workholding can be equally deceptive. A thin component may inspect correctly while clamped and move out of tolerance after release. Removing stock can redistribute residual stress, while excessive clamping force can introduce temporary deformation. Good dimensional results in the fixture do not automatically describe the delivered part.
Inspection should reflect the specified acceptance state, including release from the fixture and any relevant downstream operations. Deburring deserves particular attention: removing a burr can also round a functional edge or change the apparent size of a microfeature. The finishing sequence needs qualification, not just the cutting cycle.
Measurement uncertainty limits what can be claimed
A display showing additional decimal places does not establish adequate measurement capability. Probe geometry, contact force, optical edge detection, surface reflectivity, calibration, alignment, and temperature all influence the result. For a deep microfeature, the instrument may not access the surface that controls function.
Contact measurement can deform delicate structures or miss details because of probe-tip geometry. Optical measurement avoids contact but may respond differently to reflective surfaces, steep walls, and burrs. Computed tomography can provide access to internal geometry, but its suitability depends on material, part size, resolution, and a validated uncertainty assessment.
ISO 14253-1 addresses decision rules for proving conformity or nonconformity while accounting for measurement uncertainty. The practical consequence is simple: a reading just inside a tolerance boundary may not provide sufficient evidence of conformity under the applicable rule. Supplier and customer should agree on that rule before acceptance disputes arise.
Repeated measurements on one instrument reveal repeatability, not the entire uncertainty budget. A stronger assessment considers calibration, bias, reproducibility, environmental effects, and the suitability of the measurement strategy. Independent verification is useful, provided both methods evaluate the same measurand.
Benchmark the process window, not the best part
A practical error budget separates systematic offsets, time-dependent drift, and random variation. Some offsets can be compensated; unstable behavior usually requires a process change. Simply adding every maximum error may be overly conservative, while root-sum-square combination is not automatically justified when contributions are correlated or poorly characterized.
For supplier evaluation, request evidence that exposes those distinctions:
- Representative geometry: the actual material, feature depth, wall thickness, datum scheme, and finishing sequence.
- Time-ordered results: measurements covering relevant thermal conditions, tool wear, and setup changes, rather than selected passing parts.
- Inspection definition: equipment, sampling strategy, uncertainty assessment, and agreed acceptance rule.
- Reaction plan: criteria for compensation, tool replacement, reinspection, and containment after detected drift.
Capability indices are useful only when their assumptions and sampling basis are credible. A high Cpk calculated from a short, unstable, or selectively screened run does not establish dependable production capability. Ask whether the evidence represents one setup, several tool changes, or the full manufacturing route.
This distinction also matters in cross-sector benchmarking. Global Industrial Matrix (GIM) connects precision tooling with electronics, mobility, and other manufacturing systems, where comparable claims require comparable definitions. An IATF 16949-certified quality system or an applicable IPC requirement can provide relevant context, but neither substitutes for feature-specific machining and inspection evidence.
The achievable tolerance in micro precision machining is ultimately the tolerance that remains demonstrable after thermal change, tool wear, unclamping, finishing, and measurement uncertainty are considered. If a supplier can show only a machine specification or one exceptional part, the limit has not yet been established. Qualify the most demanding functional feature under realistic production conditions—and use that evidence to decide whether to tighten the process, relax the drawing, or change the manufacturing route.

The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.