Monday, May 22, 2024
How to vet tooling insights and expert opinions on mold wear
by
Published
Views:
How to vet tooling insights and expert opinions on mold wear
When mold wear starts affecting dimensional accuracy, surface finish, or production uptime, which recommendations deserve your trust? Confident diagnoses are easy to find. Reliable ones connect a documented defect to a plausible wear mechanism, then explain why a particular intervention should work under your production conditions.
Vetting tooling insights and expert opinions therefore means examining measurement methods, operating history, material compatibility, and the limits of the evidence. The decision is not simply whether an expert sounds credible. It is whether the assessment supports maintenance, refurbishment, or replacement without introducing a larger risk elsewhere.
Global Industrial Matrix (GIM) approaches technical benchmarking through verifiable data and cross-sector comparison. That perspective is useful here: tooling condition cannot be separated from processing, product requirements, maintenance practices, and supply-chain constraints. A recommendation should survive scrutiny across all four.
Establish what is actually changing
Before comparing supplier opinions, write a precise description of the problem. “The mold is worn” is a conclusion, not an observation. More useful statements identify the affected cavity, feature, defect, operating state, and trend: flash developing at a particular shutoff, a surface defect recurring after cleaning, or a dimension drifting under otherwise stable conditions.
Part measurements alone do not prove tool wear. In injection molding, dimensional drift can also reflect resin conditioning, packing, cooling, or machine variation. Flash may involve damaged parting surfaces, but alignment and clamping conditions also need checking. In die casting, soldering, erosion, and thermal fatigue require different investigations. These mechanisms should not be treated as interchangeable.
Build a shared evidence packet before requesting proposals:
- Tool drawings, revision history, cavity identification, and critical product tolerances.
- Tool steel, heat treatment, coatings, and previous repairs, where documented.
- Production material, including reinforcement or additives relevant to abrasion or corrosion.
- Cycle history, process records, maintenance events, and recent changes in defect behavior.
- Part inspection results and tool measurements tied to identifiable locations.
Missing records do not automatically prevent a decision. They do change its confidence level. An expert who identifies those gaps is usually offering a more useful assessment than one who quietly assumes them away.
Test the diagnosis against the wear pattern
A credible diagnosis should explain why damage appears where it does. Abrasive wear may be consistent with filled polymers and concentrated flow paths. Corrosion may relate to material chemistry, moisture, deposits, or storage conditions. Galling at sliding interfaces points toward contact conditions, alignment, lubrication, and material pairing. Thermal checking requires attention to repeated thermal loading rather than surface appearance alone.
Ask the expert to separate three things: what was observed, what mechanism is inferred, and what remains unverified. “Pitting is visible near the vent” is an observation. “Corrosive deposits caused it” is an interpretation that needs supporting evidence. “A different steel will prevent recurrence” is a proposed remedy with additional assumptions.
Location matters as much as severity. A small change at a precision shutoff can have a larger production consequence than a broader cosmetic change elsewhere. Request an annotated map linking tool damage to affected part features, rather than accepting disconnected photographs.
The strongest assessments also consider competing explanations. If the diagnosis is abrasive wear, what evidence argues against corrosion or damage from cleaning? If misalignment is suspected, has it been measured? A recommendation becomes more dependable when it explains both the preferred interpretation and the alternatives that were ruled out.
Check whether the measurements can support the claim
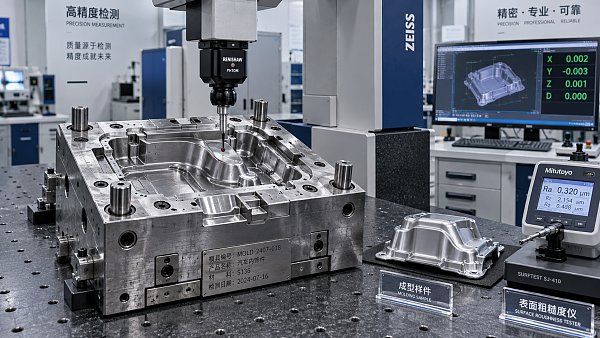
“Measured with a CMM” is not enough. The inspection report should identify the datum strategy, feature definition, measurement conditions, and relevant uncertainty. Comparing two reports with different alignments can create apparent wear that is actually a measurement-method difference.
For dimensional comparisons, ask whether the tool was measured in comparable thermal and assembly states. For surface measurements, check the parameter, measurement direction, filtering, and sampling location. A roughness result does not describe every functional aspect of a textured, polished, or coated surface.
Photographs are useful for locating damage and tracking visible changes, but lighting and magnification affect interpretation. They cannot independently establish the depth of erosion or remaining coating thickness. Those claims require a suitable measurement method, with any sampling limitations made explicit.
The practical question is whether measurement variation is small enough to distinguish the suspected change. If not, improve the inspection plan before authorizing irreversible work. Polishing, welding, or machining can remove evidence that would otherwise clarify the cause.
Evaluate expertise by relevance, not confidence
Experience transfers unevenly. An expert in high-volume thermoplastic tooling may understand abrasive wear well but have less direct experience with thermal fatigue in die-casting dies. A coating specialist may understand adhesion and surface preparation without owning the process conditions that caused the original damage.
Ask for evidence of work on comparable tooling materials, damage mechanisms, and functional requirements. Public technical papers, anonymized inspection reports, documented repair procedures, and references can help establish relevance. Confidentiality may limit disclosure; it should not prevent an explanation of the diagnostic method.
Commercial interests should also be visible. A repair shop, steel supplier, and coating provider may reasonably recommend different interventions because each sees a different part of the problem. That does not invalidate their advice. It means proposals must be compared against a shared failure definition, not against each supplier’s preferred service.
Be cautious when an opinion promises a fixed tool-life improvement without defining operating conditions, inspection intervals, or the endpoint for “life.” Cycle counts from another application are context, not a transferable guarantee.
Compare remedies by what they change—and what they leave unresolved
A proposal should identify the failure mechanism it addresses, the geometry it changes, and the verification needed afterward. The lowest repair price is not necessarily the lowest-risk decision, but replacement is not automatically justified by a visible defect either.
Repair compatibility deserves particular attention. Welding can introduce distortion and local metallurgical changes. Polishing can alter dimensions or edge geometry. Coating preparation and deposition can affect fit, while processing temperatures must be compatible with the substrate’s treatment history. None of these methods is inherently unsuitable; each needs an application-specific justification.
Compare commercial proposals on total production exposure: intervention cost, downtime, qualification effort, scrap during restart, spare-tool availability, and recurrence risk. Keep uncertain inputs visible rather than hiding them inside a single savings figure.
Use benchmarks without confusing them with proof
Cross-sector tooling insights and expert opinions can reveal useful questions about traceability, inspection discipline, and maintenance planning. They cannot establish that two tools should achieve the same life merely because their steels or coatings are similar.
GIM brings together intelligence across Semiconductor & Electronics, Automotive & Mobility, Smart Agri-Tech, Industrial ESG & Infrastructure, and Precision Tooling. For mold decisions, the value of that breadth is recognizing dependencies: a repair may restore geometry yet still affect qualification schedules, spare capacity, or downstream product acceptance.
Standards references need the same discipline. ISO, IATF, and IPC requirements may be relevant to particular quality systems or products, but citing them broadly does not validate a wear diagnosis. Ask which requirement applies, what evidence demonstrates conformity, and whether it governs the tool, the finished product, or the organization’s processes.
Make approval conditional on a verification plan
Before authorizing work, agree on the as-found record, intervention scope, acceptance criteria, and production trial. Tool inspection should verify the repaired features; part inspection should confirm functional results under a documented process window. Where appropriate, monitoring after restart should check whether the original defect returns.
Define what would trigger further action. A restored dimension does not prove long-term durability, and a short successful trial does not establish remaining tool life. If uncertainty remains, a staged intervention or controlled trial may be more defensible than an unconditional replacement decision.
The next supplier conversation should end with four clear answers: what failed, how that conclusion was reached, why the proposed remedy fits, and how success will be verified. If any answer remains vague, request the missing evidence before committing the tool—and the production schedule—to the recommendation.
The Archive Newsletter
Critical industrial intelligence delivered every Tuesday. Peer-reviewed summaries of the week's most impactful logistics and market shifts.